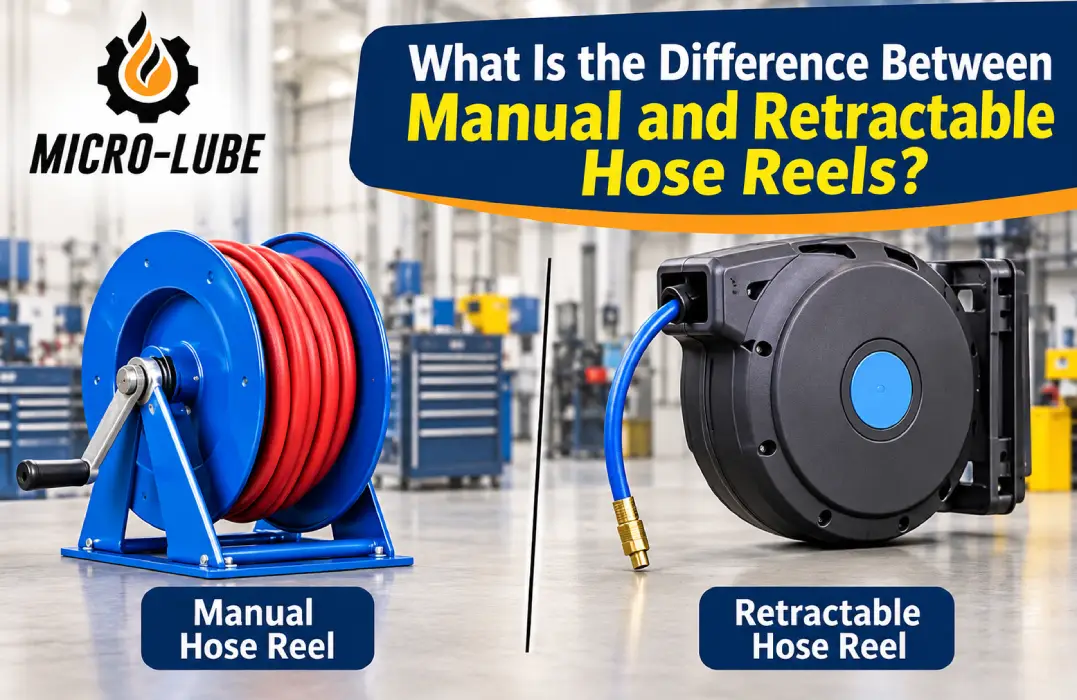
What Is the Difference Between Manual and Retractable Hose Reels?

Hose reels are essential tools for managing hoses used in industrial facilities, maintenance workshops, manufacturing plants, garages, construction sites, and equipment service areas. They help keep hoses organized, reduce clutter, simplify fluid handling, and improve workplace safety. When choosing a hose management solution, one of the most common decisions is whether to use a manual hose reel or a retractable hose reel. Although both types serve the same basic purpose—storing and managing hoses—they differ in how the hose is extended, retracted, operated, and maintained. The right choice depends on the application, hose length, frequency of use, available space, operating environment, and the type of fluid or material being transferred. Understanding the difference between manual and retractable hose reels can help businesses choose equipment that improves daily workflow, minimizes hose damage, and makes maintenance operations more efficient.

What Is a Manual Hose Reel?

A manual hose reel is a hose storage system operated by hand. It typically features a rotating drum, a frame, a crank handle, and a hose that is wound or unwound manually. The operator turns the handle to roll the hose onto the reel after use or to release the hose when needed. Manual hose reels are commonly used in workshops, maintenance facilities, industrial plants, agricultural operations, and fluid transfer stations where hose use is moderate and operators have time to manage the hose manually. These reels are often valued for their straightforward design, ease of installation, and dependable operation. Because they do not rely on automatic spring mechanisms or powered components, manual hose reels can be a practical choice for applications where simplicity and control are important.

Key Features of Manual Hose Reels

  • Hand-operated winding mechanism
  • Simple mechanical construction
  • Controlled hose extension and retraction
  • Suitable for light to moderate hose usage
  • Available for different hose lengths, diameters, and applications
  • Typically requires the operator to wind and unwind the hose
Manual hose reels can be useful when hoses need to be positioned carefully or when operators prefer to control the winding speed and tension themselves.

What Is a Retractable Hose Reel?

A retractable hose reel is designed to automatically wind the hose back onto its drum after the operator releases or activates the retraction mechanism. Most industrial retractable hose reels use an internal spring-driven mechanism, although some applications use motorized systems. The operator pulls the hose out to the required length, and the reel locks or holds it in position during use. When the hose is ready to be stored, the locking mechanism is released, allowing the reel to retract the hose in a controlled manner. Retractable hose reels are frequently used in busy maintenance workshops, manufacturing facilities, automotive service centers, fleet maintenance areas, and industrial workplaces where hoses are used regularly throughout the day.

Key Features of Retractable Hose Reels

  • Automatic hose retraction mechanism
  • Spring-powered or motorized winding system, depending on design
  • Reduced manual effort during hose storage
  • Improved hose organization
  • Convenient hose access for repetitive tasks
  • Available in wall-mounted, ceiling-mounted, and other installation configurations
Retractable hose reels are particularly beneficial in environments where operators frequently extend and store hoses and where keeping the floor clear is an important safety consideration.

Manual vs. Retractable Hose Reels: Key Differences

The main difference between manual and retractable hose reels is how the hose is managed and stored. Manual reels require the operator to turn a crank to wind the hose, while retractable reels automatically return the hose using an internal mechanism. Here is a comparison of their most important differences.
Feature Manual Hose Reel Retractable Hose Reel
Operation Hand crank Automatic retraction
Hose storage Operator winds hose Internal mechanism winds hose
Physical effort More manual effort Less manual effort
Hose retrieval Controlled by crank Spring or motor mechanism
Best suited for Occasional or planned use Frequent, repetitive use
Maintenance Simple mechanical components Requires mechanism inspection
Convenience Basic and dependable Faster and more convenient
Installation Wall, floor, or other mounting Wall, ceiling, or other mounting
Hose control Operator controls winding Retraction mechanism controls winding
Workplace application General maintenance and transfer High-activity service areas

1. Ease of Operation

Manual hose reels require the operator to turn a crank to wind the hose back onto the drum. This process is straightforward but can take additional time, especially when handling long or heavy hoses. In applications where hoses are used only occasionally, the manual operation may not create a significant inconvenience. Retractable hose reels simplify this process by automatically winding the hose back onto the reel. The operator only needs to guide the hose during retraction, depending on the reel design. This makes hose storage easier and more convenient, particularly when equipment is used multiple times during a shift. For workplaces where hose handling is frequent, retractable hose reels can reduce repetitive manual effort and help employees complete maintenance tasks more efficiently.

2. Productivity and Workflow Efficiency

Hose management can directly affect how quickly maintenance personnel complete their work. Operators who regularly transfer oil, dispense lubricants, supply air, wash equipment, or perform maintenance may spend considerable time pulling out, repositioning, and storing hoses. Manual hose reels work well when hose usage is less frequent or when operators need a simple storage solution. However, winding hoses manually after every task can add time to repetitive maintenance activities. Retractable hose reels can help improve workflow by allowing the hose to be stored quickly after use. In busy workshops and industrial service stations, this convenience can make work areas easier to manage and reduce unnecessary interruptions between tasks.

3. Hose Protection and Durability

Hoses can deteriorate prematurely when they are dragged across rough floors, exposed to sharp edges, twisted, bent excessively, or stored improperly. Poor hose storage can lead to abrasion, kinking, leaks, and damage to fittings. Manual hose reels allow operators to wind hoses at their preferred speed. When used correctly, they can provide organized storage and help protect hoses from unnecessary damage. However, inconsistent winding may cause the hose to overlap unevenly or become tangled. Retractable hose reels are designed to return hoses to a storage position after use. Proper retraction helps keep hoses off the floor and reduces exposure to common workplace hazards. However, operators should avoid allowing hoses to snap back uncontrolled, as this can damage hose fittings, create safety hazards, or cause unnecessary wear. Both types of hose reels can support longer hose service life when they are properly selected, installed, and operated.

4. Workplace Safety and Organization

Loose hoses on the floor can create trip hazards, interfere with equipment movement, and make maintenance areas difficult to navigate. This is particularly concerning in manufacturing facilities, vehicle maintenance workshops, and industrial environments where employees move tools, machinery, carts, and materials throughout the day. Manual hose reels improve organization by providing a dedicated location for hose storage. However, employees must remember to wind and store the hose after each use. Retractable hose reels make hose storage more convenient and help keep hoses elevated and out of walkways. This can support better workplace organization, reduce hose clutter, and make equipment easier to access. The benefits of either reel depend on employees following proper hose handling procedures and ensuring hoses are stored correctly after each task.

5. Maintenance Requirements

Manual hose reels generally have fewer mechanical components than automatic retractable reels. Their maintenance requirements may include inspecting the drum, crank handle, frame, bearings, mounting hardware, hose, and connections. Regular inspection helps identify wear, corrosion, loose fittings, or mechanical issues before they affect operation. Retractable hose reels require additional attention to the spring assembly, locking mechanism, retraction system, hose guide, and other moving components. The mechanism should be inspected periodically to ensure the hose retracts smoothly and does not release unexpectedly. Maintenance requirements vary by manufacturer, reel construction, operating conditions, and frequency of use. Choosing a reel that is suitable for the working environment can help reduce unnecessary repairs and improve reliability.

6. Cost and Long-Term Value

Manual hose reels are often an attractive choice for businesses looking for a straightforward hose management solution. Their simple design may offer lower initial costs and fewer mechanism-related maintenance concerns. Retractable hose reels may require a higher initial investment, depending on hose specifications, construction materials, mounting requirements, and retraction mechanism. However, businesses with frequent hose use may benefit from reduced manual handling, improved convenience, and better organization. Rather than comparing purchase price alone, businesses should evaluate the total cost of ownership, including installation, maintenance, hose replacement, operator time, and workplace efficiency. A cost-effective hose reel is one that meets the application’s requirements without introducing unnecessary complexity or sacrificing performance.

When Should You Choose a Manual Hose Reel?

A manual hose reel is a suitable option when hose use is occasional, the hose length is manageable, and operators do not need to retract the hose repeatedly throughout the day. Consider a manual hose reel if:
  • Hose usage is limited to occasional maintenance or transfer operations.
  • A simple, straightforward hose storage system is preferred.
  • Operators need controlled winding and unwinding.
  • The facility wants a practical hose organization solution.
  • The application does not require frequent automatic hose retraction.
Manual hose reels can be a good fit for small workshops, equipment service areas, storage facilities, and maintenance locations where simplicity is more important than rapid hose retrieval.

When Should You Choose a Retractable Hose Reel?

Retractable hose reels are often a better option for high-activity environments where hoses are used frequently and need to be stored quickly after every task. Consider a retractable hose reel if:
  • Employees use hoses multiple times throughout the workday.
  • The workplace needs to minimize hose clutter.
  • Faster hose storage is important for workflow efficiency.
  • Operators want to reduce repetitive manual winding.
  • The hose needs to remain organized and accessible between tasks.
Retractable hose reels are commonly used in industrial facilities, fleet maintenance shops, manufacturing plants, automotive service centers, and equipment maintenance areas.

How to Choose the Right Hose Reel for Your Application

Before purchasing a manual or retractable hose reel, evaluate the specific requirements of your facility. Selecting the wrong reel can result in poor hose handling, insufficient capacity, premature hose wear, and unnecessary maintenance. Consider these factors:
  • Hose length: Select a reel that can accommodate the required hose length without overfilling the drum.
  • Hose diameter: Ensure the reel is compatible with the hose size and required flow rate.
  • Fluid compatibility: Choose a reel, hose, and fittings suitable for the fluid being handled, such as oil, grease, air, water, or other approved materials.
  • Operating pressure: Confirm that the hose reel and associated components are rated for the application’s working pressure.
  • Mounting location: Determine whether wall, ceiling, floor, or equipment mounting is appropriate.
  • Frequency of use: Consider how often operators extend and retract the hose during daily operations.
  • Workplace conditions: Evaluate exposure to dust, moisture, temperature variations, chemicals, and mechanical impact.
  • Maintenance requirements: Choose equipment that can be inspected and maintained according to the facility’s capabilities.
Evaluating these factors helps businesses select hose reels that support reliable operation, safer handling, and efficient fluid management.

Frequently Asked Questions

1. Are retractable hose reels better than manual hose reels?

Retractable hose reels are generally more convenient for frequent hose use because they automatically wind the hose back into storage. Manual hose reels can be more practical for occasional applications where simplicity and lower initial cost are priorities.

2. Do manual hose reels require electricity?

No. Manual hose reels operate using a hand crank and do not require electricity. Retractable hose reels can also operate without electricity if they use a spring-powered mechanism, while motorized versions require a power source.

3. Can retractable hose reels be used for oil transfer?

Yes. Retractable hose reels designed and rated for compatible oils and operating pressures can be used in industrial oil dispensing and transfer applications. The hose, seals, fittings, and reel materials must be suitable for the oil being handled.

4. Which hose reel is best for industrial workshops?

The best option depends on hose usage, workspace layout, operating requirements, and maintenance needs. Retractable reels are often preferred in busy workshops, while manual reels can be suitable for occasional use or simpler applications.

5. Do retractable hose reels prevent hose damage?

Retractable hose reels can help reduce hose damage by keeping hoses organized and off the floor. However, proper hose selection, controlled retraction, regular inspection, and correct operation are still essential for preventing premature wear.

Conclusion

Manual and retractable hose reels both play an important role in industrial hose management. Manual reels provide simple, controlled hose storage with a hand-operated winding mechanism, while retractable hose reels offer automatic hose retrieval, convenience, and improved organization for frequent-use applications. Choosing between them depends on the frequency of hose use, workplace layout, fluid compatibility, operating pressure, maintenance requirements, and long-term cost considerations. Selecting the right hose reel can help reduce hose wear, improve workplace safety, and make daily maintenance and fluid handling tasks more efficient. Micro-Lube provides industrial fluid handling and lubrication equipment designed to support efficient maintenance operations across the USA and Canada. Explore Micro-Lube’s hose reel solutions and fluid handling products to find equipment that matches your application, or contact Micro-Lube for assistance in selecting the right hose management solution for your facility.

How Do You Choose the Right Lubrication System for Heavy Equipment?

Heavy equipment plays an essential role in construction, mining, agriculture, transportation, and industrial operations across the United States and Canada. Machines such as excavators, bulldozers, wheel loaders, cranes, and mining trucks operate under demanding conditions. Their moving components experience continuous friction, heavy loads, vibration, dust, and changing temperatures. Without proper lubrication, these conditions can contribute to premature wear, increased maintenance requirements, and unexpected equipment downtime. Choosing the right lubrication system for heavy equipment is an important part of maintaining machine performance and reliability. A suitable system delivers the required amount of oil or grease to critical components at appropriate intervals. It also helps maintenance teams manage lubrication tasks more efficiently and maintain consistent servicing practices.

However, different machines have different lubrication requirements. Equipment size, operating environment, lubricant type, number of lubrication points, and maintenance schedules all influence the selection process. This guide explains how to choose a suitable lubrication system for heavy equipment and what businesses should consider before making a decision.

What Is a Lubrication System for Heavy Equipment?

A lubrication system supplies oil or grease to machine components that require continuous or periodic lubrication. Its primary purpose is to reduce friction between moving surfaces, control heat, and help minimize mechanical wear. Heavy equipment contains several components that depend on proper lubrication, including:
  • Bearings and rotating shafts
  • Pins and bushings
  • Pivot points and joints
  • Moving linkages
  • Gears and other mechanical connections
  • Components specified by the equipment manufacturer
Without sufficient lubrication, direct contact between moving surfaces can increase friction and temperature. Over time, this may affect component performance and lead to costly repairs. Depending on the machine and its requirements, lubrication can be performed manually or through an automatic lubrication arrangement.

1. Understand Your Equipment’s Lubrication Requirements

The first step is to understand the type of equipment you operate and the lubrication requirements of its individual components. An excavator, for example, has several moving joints around its boom, arm, bucket, and attachments. A bulldozer operates under heavy loads and challenging ground conditions, while a mining truck may work for extended shifts in dusty environments. Each machine has different lubrication points, operating cycles, and maintenance requirements. Before selecting a system, consider:
  • What type of heavy equipment needs lubrication?
  • How many lubrication points does the machine have?
  • Which components require grease, and which require oil?
  • How frequently does each component need lubrication?
  • Are the lubrication points easy to access?
  • Does the machine operate continuously or intermittently?
Reviewing the equipment manufacturer’s maintenance instructions is important. These instructions help identify the correct lubricant specifications, lubrication quantities, and recommended service intervals.

2. Select the Correct Lubricant Type

Lubricant selection directly affects the performance of a lubrication system. Heavy equipment commonly uses oil or grease, depending on component design and operating requirements.

Grease Lubrication

Grease is frequently used for bearings, pins, bushings, joints, and other components where the lubricant needs to remain around the contact surfaces. It is particularly useful in applications where grease retention is important. However, grease consistency must match the requirements of the equipment and lubrication system. Before selecting grease, consider its consistency, operating temperature range, compatibility with the system, and ability to move through the delivery lines.

Oil Lubrication

Oil is used in applications where liquid lubrication is required. It may be supplied through dedicated lubrication arrangements or circulation systems, depending on the equipment design. The correct oil viscosity is important because it affects how the lubricant flows and forms a protective film between moving surfaces. Always follow the lubricant specifications recommended for the equipment. Using an unsuitable oil or grease can affect delivery performance and may contribute to inadequate lubrication.

3. Evaluate the Number and Location of Lubrication Points

The number of lubrication points is another important factor when choosing a system. Smaller machines with only a few accessible lubrication points may be maintained using manual lubrication equipment. However, larger machines with multiple lubrication points may benefit from a centralized or automatic lubrication arrangement. Consider a wheel loader that operates throughout the day. Its moving joints and bearings require regular attention. If maintenance technicians must manually reach every lubrication point, servicing may take considerable time. An appropriate centralized system can deliver lubricant through connected lines to selected lubrication points, reducing the need for repeated manual application. When evaluating lubrication points, identify:
  • The total number of points requiring lubrication.
  • The location of each point.
  • The required lubricant quantity.
  • The lubrication frequency.
  • The accessibility of each component.
  • The distance between the lubricant reservoir and delivery points.
A lubrication-point diagram can help maintenance teams understand the system layout and plan an appropriate installation.

4. Compare Different Types of Lubrication Systems

There are several lubrication system designs available for industrial and heavy-duty applications. Each has different operating characteristics and may be suitable for specific equipment requirements.

Manual Lubrication Systems

Manual lubrication involves applying grease or oil using suitable tools, such as grease guns or oil dispensers. This approach may be practical for smaller machines or equipment with a limited number of lubrication points. It also provides technicians with direct control over the lubrication process. However, manual servicing requires regular attention. If maintenance schedules are missed or lubrication points are difficult to reach, some components may not receive lubricant at the required intervals.

Single-Line Lubrication Systems

Single-line systems distribute lubricant through a main supply line connected to suitable metering devices or injectors. They can be considered for applications where the number of lubrication points, lubricant requirements, and system layout are compatible with this design. The system must be correctly sized to ensure that lubricant reaches the intended points.

Progressive Lubrication Systems

Progressive lubrication systems distribute lubricant through a sequence of metering components. Each component operates in a defined order to deliver lubricant to connected points. These systems are often considered for machinery with multiple lubrication points that require controlled lubricant delivery. Because the distribution components operate in sequence, an interruption or blockage can affect the lubrication cycle. Appropriate monitoring and regular inspection are therefore important.

Dual-Line Lubrication Systems

Dual-line lubrication systems use two main supply lines that are pressurized alternately to operate distribution devices. They can be suitable for larger installations with numerous lubrication points and more extensive distribution networks. The selection depends on the required lubricant volume, operating pressure, equipment layout, and application. The best system is the one that matches the machine’s actual lubrication requirements rather than simply choosing the most complex design.

5. Consider Weather and Operating Conditions

Heavy equipment used in the United States and Canada often operates in different climates and working environments. Temperature, dust, moisture, and vibration can all influence lubrication system performance.

Cold Weather Conditions

In colder regions, low temperatures can make some lubricants thicker and more difficult to move through delivery lines. Equipment operating in northern Canada or colder parts of the United States may require a lubrication arrangement compatible with the expected temperature range.

Hot Weather Conditions

High temperatures can affect lubricant properties and increase the demands placed on equipment components. Machines working in hot environments may require suitable lubricant specifications and more frequent condition checks, depending on operating conditions.

Dusty and Wet Environments

Construction sites, mining operations, and agricultural facilities often expose equipment to dirt, dust, mud, and moisture. Contamination can affect lubricant quality and contribute to component wear. Suitable protection, clean lubricant handling practices, and regular inspections help maintain system performance. Before selecting a lubrication system, evaluate the actual working environment rather than relying only on general equipment specifications.

6. Check Pump Capacity and Delivery Requirements

For an automatic lubrication system, the pump must be capable of supplying the required lubricant to the distribution network. Selecting an unsuitable pump can result in inconsistent lubricant delivery or an inability to meet the system’s operating requirements. Important factors include:
  • Total number of lubrication points.
  • Required lubricant quantity at each point.
  • Lubricant viscosity or grease consistency.
  • Required operating pressure.
  • Length and layout of delivery lines.
  • Reservoir capacity.
  • Lubrication cycle frequency.
The pump must also be compatible with the lubricant being used. Hoses, fittings, metering devices, and other components should be selected as part of a complete system. Correct system sizing helps ensure that lubricant reaches the intended components without creating unnecessary operating difficulties.

7. Look for Monitoring and Control Features

Monitoring and control features can make lubrication system management easier, especially when heavy equipment operates for long hours. Depending on the system design, available features may include timers, cycle indicators, pressure monitoring devices, low-level alerts, and electronic controllers. These features can help operators and maintenance technicians identify potential problems, such as:
  • Low lubricant levels.
  • Interrupted lubrication cycles.
  • Blocked or damaged delivery lines.
  • Pump operating problems.
  • Unusual pressure conditions.
Monitoring is particularly useful when equipment operates at remote construction or mining sites, where regular manual checks may be difficult. However, monitoring features should be selected according to the machine’s requirements. A practical system with appropriate controls is often more useful than an unnecessarily complicated installation.

8. Consider Installation and Maintenance Requirements

A lubrication system should be easy to install, inspect, refill, and maintain. Poor installation planning can create problems even when the selected equipment is technically suitable. Before installation, identify suitable mounting locations for the pump and lubricant reservoir. Delivery lines should be routed safely and protected from excessive heat, mechanical damage, and moving equipment components. Maintenance teams should have convenient access to:
  • Lubricant reservoirs and refill connections.
  • Pumps and distribution components.
  • Hoses, fittings, and delivery lines.
  • Electrical connections and controllers.
  • Filters, where required by the system design.
Routine inspections should include checking for leaks, damaged hoses, loose fittings, contamination, and unusual system behavior. Automatic lubrication does not eliminate maintenance responsibilities. It changes how lubricant is delivered, but the system itself still needs regular attention.

9. Evaluate the Total Cost of Ownership

The initial purchase price should not be the only factor when choosing a lubrication system. Businesses should also evaluate installation expenses, labour requirements, lubricant consumption, servicing costs, replacement components, and the potential impact of equipment downtime. For example, manual lubrication may require less initial investment, but it involves ongoing technician or operator time. An automatic lubrication system may have higher installation costs but can reduce repetitive manual tasks and support consistent lubricant delivery when correctly designed and maintained. A practical cost evaluation should include:
  • Initial system and installation costs.
  • Labour required for lubrication.
  • Lubricant consumption.
  • Routine inspection and maintenance.
  • Replacement parts and repairs.
  • Potential downtime and maintenance savings.
The right choice should balance system performance, reliability, maintenance requirements, and long-term operating costs.

Common Mistakes to Avoid When Choosing a Lubrication System

Selecting the wrong lubrication arrangement can create additional maintenance challenges. Avoid these common mistakes:
  1. Ignoring equipment specifications: Always check the manufacturer’s lubrication recommendations before selecting a system.
  2. Using the wrong lubricant: Incorrect oil viscosity or grease consistency can affect lubricant delivery.
  3. Overlooking lubrication points: Every required lubrication point should be identified during system planning.
  4. Choosing an unsuitable pump: Pump capacity and operating pressure must match the application.
  5. Ignoring environmental conditions: Temperature, dust, moisture, and vibration can influence system performance.
  6. Skipping regular inspections: Automatic systems still require maintenance and monitoring.
  7. Focusing only on initial cost: Consider installation, labour, servicing, and long-term operating expenses.
Avoiding these mistakes can help businesses choose a system that supports reliable equipment maintenance.

Practical Checklist for Selecting a Heavy Equipment Lubrication System

Before making a final decision, review the following factors:
Selection factor What to consider
Equipment type Excavator, bulldozer, loader, mining truck, or other machinery
Lubricant type Manufacturer-approved oil or grease
Lubrication points Number, location, and required lubricant quantity
System design Manual, single-line, progressive, or dual-line
Operating environment Temperature, dust, moisture, and vibration
Pump capacity Required pressure and lubricant delivery
Monitoring Suitable indicators, alarms, and controls
Maintenance Inspection, refilling, and servicing access
Budget Installation and long-term operating expenses
Reviewing these factors makes it easier to identify a lubrication system that matches the equipment and its working conditions.

Frequently Asked Questions

1. What is the best lubrication system for heavy equipment? The best system depends on equipment design, lubricant requirements, the number of lubrication points, and operating conditions. Manual systems may suit machines with fewer lubrication points, while automatic systems can be useful for larger equipment that requires frequent and consistent lubrication. 2. Are automatic lubrication systems suitable for construction equipment? Yes. Automatic lubrication systems can be suitable for excavators, bulldozers, wheel loaders, and other construction equipment. They can deliver measured quantities of lubricant to selected components at scheduled intervals, provided the system is correctly designed for the machine. 3. How often should heavy equipment be lubricated? Lubrication frequency depends on the equipment manufacturer’s recommendations, operating hours, component requirements, lubricant type, and working environment. Always follow the recommended maintenance schedule and inspect equipment regularly. 4. What is the difference between manual and automatic lubrication? Manual lubrication requires an operator or technician to apply lubricant to individual points. Automatic lubrication uses a pump and distribution components to supply lubricant according to a defined cycle or control arrangement. 5. Why is lubricant selection important for heavy machinery? The correct lubricant helps reduce friction, control heat, and protect moving surfaces. Incorrect viscosity or grease consistency can affect lubricant delivery and component protection, potentially increasing wear and maintenance requirements.

Conclusion

Choosing the right lubrication system for heavy equipment requires careful consideration of machine design, lubricant specifications, lubrication points, operating conditions, pump capacity, and maintenance requirements. Whether a business operates construction machinery, mining equipment, agricultural vehicles, or industrial machines, the objective is to deliver the correct lubricant to the right components at suitable intervals. A properly selected and maintained lubrication system can support equipment reliability, reduce repetitive manual work, and improve maintenance planning. Businesses operating across the United States and Canada should evaluate both their current equipment requirements and long-term operating conditions before making a decision. Micro-Lube provides industrial lubrication equipment and fluid management solutions to help businesses manage their lubrication requirements. Visit Micro-Lube or contact its team to learn more about suitable solutions for your operation.

What Is a Vacuum Dehydration System, and When Should Industries Use One?

Industrial equipment depends on clean, dry oil to maintain reliable performance and reduce unnecessary maintenance. However, water can enter industrial lubricants through condensation, leaking seals, humid air, damaged cooling systems, or improper oil storage. If moisture accumulates, it can contribute to corrosion, lubricant degradation, equipment wear, and unplanned downtime. A vacuum dehydration system is an industrial oil treatment unit that removes water from oil using controlled heating and reduced pressure. It helps reduce dissolved and emulsified moisture that conventional particle filters may not remove effectively. Depending on its design, the system may also include filtration to remove solid contaminants. For manufacturing plants, power generation facilities, mining operations, and other industrial businesses in the United States and Canada, vacuum dehydration can be an important part of an oil maintenance strategy. It is particularly useful when moisture contamination repeatedly affects hydraulic oil, turbine oil, compressor oil, or other industrial lubricants.

What Is a Vacuum Dehydration System?

A vacuum dehydration system, also known as a vacuum dehydrator or vacuum oil purification unit, is designed to separate water from industrial oil so the lubricant can potentially be returned to service. The system creates a low-pressure environment in which moisture can evaporate at a lower temperature than it would under normal atmospheric pressure. The resulting water vapor is removed from the treatment chamber, while the treated oil continues through the unit. Many industrial systems combine several components, including an oil circulation pump, heating elements, a vacuum chamber, a moisture separation mechanism, and filtration equipment. These components work together to reduce water contamination and, where suitable filters are installed, improve oil cleanliness. Vacuum dehydration may be used in applications involving:
  • Hydraulic oil reservoirs and power units
  • Turbine lubrication systems
  • Industrial compressors and gearboxes
  • Manufacturing and metal processing equipment
  • Mining and heavy machinery
  • Paper and pulp production facilities
  • Industrial oil storage tanks
  • Other equipment that requires moisture-controlled lubricants
The appropriate system depends on the lubricant type, operating temperature, water concentration, oil volume, and required treatment rate.

How Does a Vacuum Dehydration System Work?

A vacuum dehydration system removes moisture through a controlled oil treatment process. Although designs differ between manufacturers, most systems follow several basic stages.

1. Contaminated Oil Enters the System

A pump draws oil from a reservoir, storage tank, or compatible process connection. Depending on the equipment design, the oil may pass through an initial filter that captures larger solid contaminants before entering the dehydration chamber. This initial stage helps prepare the oil for treatment and can protect internal components from excessive particulate contamination.

2. The Oil Is Heated to a Controlled Temperature

The system heats the oil within a suitable operating range. Controlled heating encourages moisture to evaporate more efficiently under vacuum conditions. Temperature control is important because excessive heat can damage sensitive lubricants or accelerate oxidation. The operating temperature should therefore match the equipment manufacturer’s recommendations and the properties of the oil being processed.

3. A Vacuum Helps Moisture Evaporate

The oil enters a chamber where pressure is reduced. Under these conditions, water can vaporize at a lower temperature. Many systems distribute the oil across internal surfaces or specialized components to increase the surface area exposed to the vacuum. This helps moisture escape from the oil, including dissolved water that may not be visible during a routine inspection.

4. Moisture Vapor Is Separated

The vacuum equipment removes the water vapor from the chamber. Depending on the design, the vapor may pass through a condenser, where it cools and becomes liquid for collection and appropriate disposal. The effectiveness of this stage depends on the unit’s capacity, operating conditions, and the amount and form of moisture present in the oil.

5. Treated Oil Is Filtered and Returned

After dehydration, the oil may pass through a suitable filter before returning to the reservoir or storage tank. This additional filtration stage can remove solid particles that may otherwise continue circulating through the equipment. Oil sampling and laboratory testing help confirm whether the treatment has achieved the required moisture level and particle cleanliness. Important: Vacuum dehydration primarily addresses water contamination. It does not automatically remove every contaminant or restore oil that has suffered severe chemical degradation.

When Should Industries Use a Vacuum Dehydration System?

Industries should consider vacuum dehydration when oil testing identifies excessive moisture, water repeatedly enters a lubrication system, or equipment requires stricter moisture control.

1. When Oil Testing Identifies Excessive Moisture

Water contamination is not always visible. Oil can contain dissolved water even when it appears clear, while higher moisture concentrations may produce a cloudy appearance or visible water separation. Regular oil analysis helps maintenance teams identify moisture levels before contamination creates more serious problems. Vacuum dehydration is worth evaluating when testing shows that moisture levels exceed the lubricant or equipment manufacturer’s recommended limits.

2. When Water Repeatedly Enters Hydraulic Systems

Hydraulic systems depend on oil to transmit power, lubricate components, and help control operating temperatures. Water contamination can contribute to corrosion, poor lubrication, additive problems, and damage to sensitive components. Moisture may enter through damaged seals, maintenance activities, condensation, or contaminated replacement oil. A vacuum dehydration system can help remove accumulated moisture, while proper sealing, tank maintenance, and clean oil-handling practices help prevent the problem from returning.

3. When Protecting Turbines and Other Critical Equipment

Power generation facilities and industrial plants often operate equipment that depends on consistent lubricant quality. Turbine bearings, compressors, gearboxes, and other critical components may be vulnerable to moisture-related damage. For these applications, controlling water contamination can help reduce corrosion risks and support dependable operation. Vacuum dehydration may be especially useful when oil reservoirs contain significant volumes of lubricant and routine moisture removal is insufficient.

4. When Extending the Useful Life of Industrial Oil

Industrial lubricant replacement can involve substantial costs, particularly when equipment requires large reservoirs or specialized oil grades. Removing moisture and filtering suitable oil may help facilities keep lubricants in service for longer. However, dehydration is not a substitute for oil condition monitoring. If the oil has excessive oxidation, depleted additives, or other forms of irreversible degradation, replacement may still be necessary.

5. When Conventional Filtration Is Not Enough

Standard particulate filters are designed primarily to capture solid contaminants such as dirt, wear particles, and other debris. They generally do not remove dissolved water from oil. If particle filtration keeps the oil clean but moisture remains above acceptable levels, a vacuum dehydration system may provide the additional treatment needed. Facilities should select a solution based on the specific contamination problem rather than assuming that one filtration technology can address every type of contaminant.

What Are the Benefits of Vacuum Dehydration?

A properly selected and maintained vacuum dehydration system can offer several benefits for industrial maintenance teams.

Reduced Water Contamination

The main benefit is the reduction of moisture in oil. Lower water levels can help minimize moisture-related corrosion and protect lubricant performance.

Improved Lubricant Condition

Excessive moisture can interfere with lubrication and contribute to oil degradation. Controlling water contamination helps support suitable operating conditions for many industrial lubricants.

Better Equipment Reliability

Moisture management can help reduce contamination-related problems in hydraulic systems, turbines, compressors, and other oil-lubricated machinery.

Potentially Longer Oil Service Life

When oil remains chemically suitable for reuse, removing moisture may help extend its service life and reduce the need for premature replacement.

Lower Oil Disposal Costs

Reconditioning suitable oil may reduce lubricant waste and the cost of purchasing replacement oil. Actual savings depend on the volume of oil treated, equipment costs, energy consumption, and maintenance requirements.

Support for Preventive Maintenance

Integrating dehydration with regular oil sampling and contamination monitoring allows maintenance teams to make informed decisions based on actual oil condition rather than relying only on fixed replacement schedules. These benefits are not guaranteed in every application. Results depend on oil condition, contamination levels, system design, and operating practices.

Vacuum Dehydration vs. Conventional Oil Filtration

Vacuum dehydration and conventional oil filtration are designed to address different contamination challenges.
Feature Vacuum Dehydration System Conventional Oil Filter
Primary purpose Reduce moisture in oil Remove solid particles
Dissolved water removal Designed to reduce dissolved moisture Standard particle filters generally do not remove it
Emulsified water removal Can reduce moisture, depending on system design and conditions Depends on the filtration technology
Dirt and wear particles Requires suitable integrated filtration Designed primarily for particle removal
Common application Moisture control and oil conditioning Maintaining oil cleanliness
For many industrial facilities, these technologies work best together. A vacuum dehydration unit with suitable particulate filtration can help address moisture and solid contamination during the same treatment process. However, not every application requires both technologies in one unit. Equipment selection should be based on oil analysis, contamination type, required cleanliness levels, and the operating requirements of the machinery.

How to Choose the Right Vacuum Dehydration System

Selecting suitable equipment requires an understanding of the facility’s lubricant requirements and contamination challenges. Consider these factors before choosing a system: 1. Type of oil: Hydraulic oil, turbine oil, gear oil, and compressor oil can have different viscosity and temperature requirements. Confirm that the system is compatible with the lubricant. 2. Moisture concentration: Oil testing can help establish the current water content and determine whether the contamination is dissolved, emulsified, or present as free water. 3. Oil volume and flow rate: The equipment should provide sufficient treatment capacity for the reservoir size and the time available for maintenance. 4. Filtration requirements: Determine whether integrated filters are required to remove solid particles and meet the equipment’s cleanliness specifications. 5. Operating temperature: Confirm that the unit can treat the oil without exceeding suitable temperature limits or damaging its additives. 6. Installation and portability: Consider available floor space, electrical supply, reservoir access, and whether a stationary or portable unit would better suit the facility. 7. Maintenance and monitoring: Evaluate filter replacement requirements, access to sampling points, control systems, and the availability of technical support. 8. Operating costs: Consider energy use, maintenance labor, consumables, and potential savings from reducing unnecessary oil replacement. Facilities with large quantities of free water or unusually high moisture contamination may need preliminary separation or a different treatment approach. Consulting a filtration specialist can help identify the most appropriate solution.

How Can Industries Prevent Water Contamination in Oil?

Vacuum dehydration can help manage existing moisture, but preventing water from entering the system is equally important. Industrial maintenance teams can reduce contamination risks by following these practices:
  • Inspect seals, gaskets, tank covers, and cooling equipment for leaks.
  • Keep oil storage containers clean, sealed, and protected from moisture.
  • Use suitable breathers to help limit moisture and airborne particles entering reservoirs.
  • Store replacement lubricants in appropriate conditions.
  • Use clean, dedicated equipment when transferring oil.
  • Monitor water content through regular oil analysis.
  • Investigate recurring moisture contamination rather than repeatedly treating the oil without correcting the source.
  • Maintain filters and oil-handling equipment according to manufacturer recommendations.
Combining preventive measures with condition monitoring and suitable oil purification equipment provides a more effective long-term strategy than relying on dehydration alone.

Frequently Asked Questions

1. What is the main purpose of a vacuum dehydration system?

The primary purpose is to remove water from industrial oil by using reduced pressure and controlled heating. It helps lower dissolved and emulsified moisture levels, depending on the equipment design and operating conditions.

2. Can vacuum dehydration remove dissolved water from oil?

Yes. Vacuum dehydration is designed to reduce dissolved moisture by allowing water to evaporate under reduced pressure. The amount removed depends on the oil type, initial water concentration, temperature, vacuum level, and system capacity.

3. Which industries benefit from vacuum dehydration systems?

Power generation, manufacturing, mining, steel production, pulp and paper processing, and other industries may benefit when their equipment depends on moisture-sensitive lubricants. Typical applications include hydraulic systems, turbines, compressors, and industrial gearboxes.

4. Does vacuum dehydration remove dirt and other particles?

Not by itself in every configuration. Solid particles are normally removed through suitable filtration. Some vacuum dehydration systems include integrated filters, allowing moisture removal and particle filtration to occur in one treatment process.

5. How often should industrial oil be dehydrated?

There is no universal schedule. The frequency depends on water ingress, oil analysis results, reservoir size, equipment criticality, and operating conditions. Regular testing helps determine when treatment is necessary.

6. Can vacuum dehydration extend the life of industrial oil?

It can help extend the service life of oil that remains suitable for reuse by reducing moisture contamination. However, it cannot reverse all forms of oil degradation. Oil analysis should be used to determine whether the lubricant can safely remain in service.

7. Is vacuum dehydration suitable for hydraulic oil?

Yes. It can be suitable for hydraulic oil when moisture contamination is present and the equipment is compatible with the lubricant. The treatment system should be selected according to the hydraulic oil’s specifications and the machinery manufacturer’s requirements.

Conclusion

A vacuum dehydration system helps industrial facilities control water contamination in oil by using controlled heating and reduced pressure. It can be a valuable option for facilities operating hydraulic equipment, turbines, compressors, gearboxes, and other machinery where moisture control supports reliable performance. By combining suitable dehydration equipment with particulate filtration, routine oil analysis, and good storage practices, businesses can improve lubricant management and make better-informed maintenance decisions. For industrial lubrication, filtration, and fluid management solutions in the United States and Canada, Micro-Lube can help you explore options suited to your facility’s needs.

Electric vs. Pneumatic Oil Pumps: Which Is Best for Industrial Use?

Industrial facilities depend on reliable oil transfer and lubrication equipment to keep machinery operating efficiently. Choosing the right pump can improve workflow, simplify lubricant handling, and help maintenance teams control operating costs. Two common options are electric oil pumps and pneumatic oil pumps, which use different power sources to move oil from storage containers to equipment, dispensing points, or lubrication systems. But which option is best for your application? The answer depends on your oil type, required flow rate, operating environment, available utilities, and maintenance needs. For businesses across the United States and Canada, understanding these differences can help make pump selection more practical and cost-effective. In this guide, we compare electric vs. pneumatic oil pumps, explain their advantages and limitations, and outline how to select the right solution for industrial operations.

What Is an Electric Oil Pump?

An electric oil pump uses an electric motor to drive its pumping mechanism. Depending on the design, it can transfer lubricating oil from drums, tanks, or containers to machinery and dispensing equipment. Electric oil pumps are commonly considered for manufacturing facilities, automotive workshops, fleet maintenance centers, equipment service areas, and industrial lubrication applications. They are particularly useful when a dependable electrical supply is available and operators need consistent, convenient oil delivery.

Key Benefits of Electric Oil Pumps

  • Convenient operation: Electric power allows operators to transfer oil without manually pumping it.
  • Consistent performance: Properly sized pumps can provide a predictable flow rate for routine dispensing.
  • Integration options: Compatible electric pumps can work with suitable meters, hoses, reels, switches, or control systems.
  • Reduced manual effort: Electric operation can simplify repetitive oil transfer tasks.
  • Practical installation: Facilities with suitable electrical connections may not need to install a separate compressed-air supply.
Electric oil pumps are available in different configurations. For example, electric gear pumps can be suitable for transferring compatible lubricants, but the correct model depends on viscosity, temperature, pressure, and the manufacturer’s specifications.

What Is a Pneumatic Oil Pump?

A pneumatic oil pump uses compressed air to operate its pumping mechanism. Depending on the design, air pressure drives an internal piston, diaphragm, or other mechanism that moves oil through the system. Pneumatic pumps are frequently considered for industrial workshops, fleet service centers, lubrication stations, and facilities where compressed air is already available. They can be useful when operators need to dispense lubricants at multiple workstations or use air-powered equipment as part of a broader fluid-handling setup.

Key Benefits of Pneumatic Oil Pumps

  • No electric motor at the pump drive: This can be advantageous in certain installations, subject to the equipment’s design and site safety requirements.
  • Use of existing compressed air: Facilities with adequate air infrastructure may be able to integrate a compatible pneumatic pump conveniently.
  • Flexible dispensing arrangements: Suitable models can support drum-mounted systems, hoses, reels, and lubrication points.
  • Application versatility: Different pneumatic pump designs are available for different oils, viscosities, and delivery requirements.
  • Potential suitability for demanding environments: Some models are designed for specific industrial conditions, provided all operating and safety requirements are met.
Pneumatic pumps still require a suitable compressed-air supply. Air pressure, available volume, air quality, and compressor capacity all influence performance.

Electric vs. Pneumatic Oil Pumps: Key Differences

Although both pump types transfer oil, their power sources affect installation, operating expenses, maintenance, and suitability for different industrial applications.
Comparison factor Electric oil pumps Pneumatic oil pumps
Power source Electricity Compressed air
Installation Requires a suitable electrical supply Requires a suitable compressed-air supply
Operating costs Depends on electricity use, duty cycle, and maintenance Includes compressed-air generation and distribution costs
Flow control Depends on pump design and available controls Depends on pump design and air-pressure regulation
Automation Can support compatible electrical controls Can support suitable pneumatic controls
Maintenance Motor, seals, gears, and other design-specific components Air components, seals, valves, and other design-specific parts
Typical selection priority Convenient operation and electrical control Existing air infrastructure and application suitability
The comparison is general rather than universal. Pump performance depends on the specific model, and electric and pneumatic pumps may use entirely different pumping mechanisms.

1. Energy Efficiency and Operating Costs

Energy consumption is an important consideration when selecting industrial oil pumps. Electric pumps use electricity directly to power a motor, while pneumatic pumps rely on compressed air, which requires energy to generate and distribute. For facilities that operate pumps frequently or for extended periods, evaluating total energy consumption can help identify potential savings. However, the actual cost difference depends on the equipment, operating schedule, flow requirements, and local electricity rates. For US manufacturing facilities and Canadian industrial operations, compare the following before making a decision:
  • Electricity consumption during normal operation.
  • Compressed-air demand and compressor efficiency.
  • Air leaks and pressure losses in existing distribution lines.
  • Pump duty cycle and expected daily operating hours.
  • Maintenance costs over the expected service life.
Practical tip: If your facility already operates an efficient compressed-air network, a pneumatic pump may be a convenient option. If compressed air must be generated specifically for oil transfer, an electric model may offer a simpler or more economical arrangement. Calculate the total cost for your actual application rather than relying on the pump’s purchase price alone.

2. Flow Rate, Oil Viscosity, and Performance

The correct pump must handle the lubricant at the required flow rate and operating pressure. Oil viscosity is particularly important because thicker oils generally require more effort to move through pumps, pipes, hoses, and dispensing equipment. Cold weather can make lubricants more viscous, which is especially relevant for facilities operating in Canadian winters or in colder parts of the United States. Before selecting either pump type, check:
  • The oil manufacturer’s recommended operating temperature.
  • The lubricant’s viscosity at the expected operating temperature.
  • Required flow rate and discharge pressure.
  • Hose length, diameter, and restrictions.
  • The pump’s maximum viscosity and duty-cycle specifications.
Do not assume that every electric pump is faster or that every pneumatic pump can handle thicker oil more effectively. Compare the performance curves and operating limits of the actual models you are considering.

3. Installation and Workplace Requirements

Electric oil pumps need an appropriate electrical supply, suitable wiring, and any required protection for the installation environment. Their suitability may depend on voltage, motor rating, electrical classification, and the possibility of exposure to moisture or flammable vapors. Pneumatic oil pumps need an air supply with sufficient pressure and flow. Facilities should also consider air filtration, moisture management, regulators, hoses, and any additional equipment required for safe operation. In both the United States and Canada, installation should follow applicable electrical, workplace, fire-safety, and equipment requirements. If a pump will operate in a potentially hazardous location, do not assume that pneumatic operation automatically makes the complete installation safe. Verify the pump’s certification, the lubricant’s properties, the surrounding hazards, and all relevant site requirements.

4. Maintenance and Equipment Reliability

Both electric and pneumatic oil pumps require routine inspection to maintain reliable performance. The maintenance schedule depends on the pump design, lubricant, operating conditions, and manufacturer’s instructions. Electric pump maintenance may include inspecting electrical connections, seals, gears, motors, and filters where fitted. Pneumatic pump maintenance may involve checking air lines, regulators, seals, valves, and the condition of other air-operated components. For either type, operators should monitor changes in flow rate, unusual noise, leaks, overheating where applicable, and inconsistent dispensing. A preventive maintenance plan should include:
  1. Inspecting hoses, fittings, and connections for leaks or damage.
  2. Checking the lubricant for contamination and confirming compatibility with pump materials.
  3. Keeping inlet strainers and other specified components clean.
  4. Monitoring pump performance against its normal operating range.
  5. Following the manufacturer’s service and replacement recommendations.
Proper maintenance can help reduce unexpected downtime and extend the useful life of oil transfer equipment.

Which Oil Pump Is Best for Your Industry?

The best choice depends on how your facility handles oil and which utilities are available.
Choose an electric oil pump when:
  • Your facility has a suitable electrical supply.
  • You want convenient, motor-driven oil transfer.
  • Electrical controls or compatible dispensing accessories are important.
  • You want to evaluate direct electrical energy consumption.
Consider a pneumatic oil pump when:
  • Your facility already has adequate compressed air.
  • The selected model suits your oil viscosity and flow requirements.
  • You need a compatible air-powered dispensing arrangement.
  • The pump meets the safety requirements of your operating environment.

Manufacturing and Production Facilities

Manufacturing plants often need reliable oil delivery for equipment maintenance, lubrication stations, and routine servicing. Electric pumps may be practical where electrical infrastructure and suitable controls are readily available. Pneumatic pumps can also be appropriate when compressed air is accessible at the required workstations.

Automotive and Fleet Maintenance Centers

Automotive workshops and fleet service facilities may transfer lubricants from bulk storage or drums to individual vehicles and equipment. Either pump type can be suitable when matched with compatible hoses, reels, meters, and dispensing accessories.

Mining and Construction Operations

Mining and construction businesses often maintain heavy equipment in demanding conditions. Pump selection should account for lubricant viscosity, ambient temperature, equipment mobility, power availability, and contamination risks. In remote locations, available electrical power and compressed-air infrastructure may strongly influence the decision.

Agricultural and Equipment Service Facilities

Agricultural service facilities may need to transfer lubricants for tractors, harvesters, and other machinery. The most appropriate option depends on the number of machines serviced, frequency of oil transfer, and whether the installation is fixed or mobile.

How to Choose the Right Industrial Oil Pump

Before purchasing an electric or pneumatic oil pump, work through this checklist.
  • Identify the lubricant: Confirm the oil type, viscosity, temperature range, and material compatibility.
  • Determine the required flow: Estimate how much oil must be dispensed and how quickly.
  • Check operating pressure: Confirm that the pump can meet the system’s pressure requirements.
  • Review available utilities: Compare electrical supply with compressed-air capacity.
  • Consider installation conditions: Account for available space, hose routing, mobility, and environmental hazards.
  • Calculate total ownership costs: Include purchase, installation, energy, maintenance, and replacement parts.
  • Check accessories: Make sure the pump is compatible with the required hoses, reels, meters, and fittings.
  • Follow manufacturer guidance: Confirm operating limits and maintenance intervals before installation.
A pump should be selected based on the complete application rather than the power source alone. Micro-Lube existing educational content on electric lubrication pumps also highlights the importance of application requirements, system design, and operating costs when evaluating pump options.

Frequently Asked Questions

1. What is the main difference between electric and pneumatic oil pumps? An electric oil pump uses an electric motor, while a pneumatic oil pump uses compressed air. Both can transfer oil, but their installation requirements, operating costs, controls, and maintenance needs differ. 2. Are electric oil pumps better than pneumatic oil pumps? Not in every situation. Electric pumps may suit facilities that want convenient motor-driven operation and electrical control. Pneumatic pumps may be a practical choice where sufficient compressed air is already available. The best option depends on the application and the individual pump’s specifications. 3. Which pump is better for thick industrial oil? Either type may work, depending on its design and rated viscosity range. Check the lubricant’s viscosity at the actual operating temperature, required flow rate, and pump manufacturer’s specifications before purchasing. 4. Are pneumatic oil pumps cheaper to operate? Not necessarily. Their operating costs include compressed-air generation and distribution. Electric pumps consume electricity directly. Comparing both systems’ energy use, maintenance requirements, and installation costs provides a more reliable answer. 5. Can electric and pneumatic oil pumps be used in automotive workshops? Yes. Both can be suitable for automotive workshops and fleet maintenance facilities when correctly sized and installed. The decision depends on dispensing volume, available utilities, lubricant requirements, and the accessories needed. 6. What should US and Canadian businesses consider before buying an oil pump? Businesses should assess lubricant viscosity, flow rate, operating pressure, electrical or compressed-air availability, installation conditions, service requirements, and applicable safety standards. Cold-weather performance is also important for facilities operating in colder Canadian and US regions.

Conclusion

Choosing between electric and pneumatic oil pumps starts with understanding your facility’s operating requirements. Electric models can provide convenient operation and integration with compatible electrical controls, while pneumatic models can be a practical choice for facilities with an established compressed-air supply. Neither option is universally better; the right pump is the one that delivers the required flow and pressure, handles your lubricant correctly, meets site safety requirements, and offers suitable long-term operating costs. For businesses across the United States and Canada, Micro-Lube offers industrial fluid handling and lubrication equipment to help meet a range of application needs. Visit Micro-Lube to explore available products or contact the team for assistance choosing suitable oil transfer and lubrication equipment.

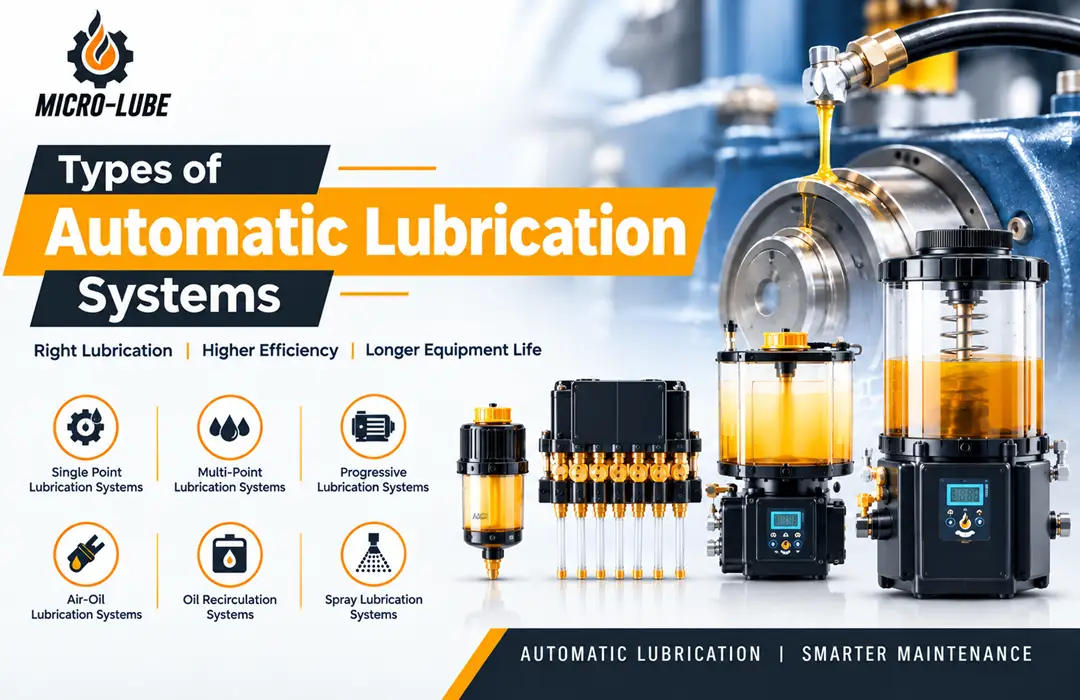
How Many Types of Automatic Lubrication Systems Are There?

Automatic lubrication systems help industrial equipment receive the right amount of lubricant at regular intervals without requiring technicians to manually lubricate every lubrication point. In manufacturing plants, mining operations, construction sites, transportation fleets, agriculture, and other demanding industries across the United States and Canada, these systems can support consistent lubrication and simplify maintenance. But how many types of automatic lubrication systems are there? The answer depends on how the systems are classified. The most common types include single-line, dual-line, progressive, and single-point lubrication systems. Some applications also use circulating oil lubrication systems and specialized systems designed for specific machinery.

Understanding how each system works can help maintenance teams select a suitable solution for their equipment, lubricant, operating environment, and number of lubrication points.

Also Read: Automatic Lubrication System Troubleshooting Guide

What Is an Automatic Lubrication System?

An automatic lubrication system delivers grease or oil to selected lubrication points automatically according to a predetermined schedule or operating condition.

A typical system includes:

  • Lubricant reservoir
  • Pump
  • Controller or timer
  • Distribution components
  • Metering devices
  • Lubrication lines
  • Fittings and connection points

Instead of relying on technicians to lubricate each bearing or component manually, the system distributes lubricant through a controlled network.

This approach can be especially useful when equipment has many lubrication points, operates continuously, or works in locations where manual access is difficult.

How Many Types of Automatic Lubrication Systems Are There?

There is no single universal classification, but four major types are commonly used in industrial applications:

  1. Single-line lubrication systems
  2. Dual-line lubrication systems
  3. Progressive lubrication systems
  4. Single-point lubrication systems

In addition, some industrial applications use circulating oil lubrication systems and specialized oil-air or air-oil systems.

Let’s look at the major types in more detail.

1. Single-Line Automatic Lubrication Systems

A single-line system uses one main supply line to deliver lubricant from the pump to metering devices. The metering devices then provide controlled amounts of lubricant to individual lubrication points.

These systems can work well for machines with relatively simple lubrication requirements.

Common applications

Single-line systems may be used for:

  • Manufacturing machinery
  • Conveyors
  • Machine tools
  • Small and medium-sized industrial equipment
  • Fans and blowers
  • General plant machinery

One advantage is the relatively straightforward system design. Maintenance teams can also configure the system according to the number and location of lubrication points.

2. Dual-Line Automatic Lubrication Systems

Dual-line systems use two main lubricant lines that alternate between supplying lubricant and returning to the pressure cycle.

This design makes dual-line systems suitable for large lubrication networks with many lubrication points.

Where are dual-line systems used?

They are commonly considered for demanding industrial environments such as:

  • Steel mills
  • Mining equipment
  • Cement plants
  • Paper mills
  • Heavy manufacturing
  • Large conveyor systems
  • Large industrial machinery

A major benefit is the ability to serve a large number of lubrication points over considerable distances.

For large facilities in the United States and Canada, where equipment may operate continuously in demanding environments, system capacity and reliability are important factors when selecting an automatic lubrication solution.

3. Progressive Automatic Lubrication Systems

Progressive lubrication systems use a series of metering devices to distribute lubricant progressively from one outlet to another.

The lubricant moves through the metering blocks in a predetermined sequence. Each outlet receives a controlled amount of lubricant before the cycle progresses.

Why use a progressive system?

Progressive systems can be useful when an application requires precise lubricant distribution across multiple points.

They are commonly used on:

  • Construction equipment
  • Mobile equipment
  • Agricultural machinery
  • Conveyors
  • Material-handling equipment
  • Industrial machinery

Another useful feature is that some progressive systems can provide monitoring information. If a blockage occurs, the system may stop or indicate an issue, depending on the configuration.

This can help maintenance teams identify lubrication problems before they cause more serious equipment issues.

4. Single-Point Automatic Lubrication Systems

Single-point automatic lubricators are designed to lubricate one lubrication point automatically.

They are often compact and easy to install, making them suitable for bearings and other components that are difficult or inconvenient to access manually.

Common applications

Single-point lubricators can be used for:

  • Electric motor bearings
  • Fans
  • Pumps
  • Small gearboxes
  • Conveyor bearings
  • Blowers
  • Other individual lubrication points

They can be particularly useful when manual lubrication would require technicians to repeatedly access elevated, enclosed, hot, or otherwise difficult-to-reach components.

5. Circulating Oil Lubrication Systems

Circulating oil systems are another important category used in industrial applications.

Instead of simply delivering a small quantity of lubricant to a lubrication point, these systems circulate oil through equipment and return it to a reservoir.

The oil can provide lubrication while also helping remove heat from certain components.

Typical applications include:

  • High-speed machinery
  • Bearings
  • Gear systems
  • Compressors
  • Turbines
  • Large industrial equipment

Filtration and oil condition management are important considerations because contaminants can affect both lubricant quality and equipment performance.

Automatic Grease vs. Automatic Oil Lubrication

Automatic lubrication systems generally use either grease or oil, depending on the equipment and application.

Feature Automatic Grease Automatic Oil
Typical use Bearings, pins, bushings Bearings, gears, circulating systems
Lubricant consistency Semi-solid Liquid
Leakage control Generally easier Requires suitable containment
Cooling capability Limited Can provide better heat transfer
Common applications Heavy-duty equipment High-speed or circulating systems

The correct lubricant depends on the manufacturer’s specifications, operating temperature, load, speed, and equipment design.

Also Read: Complete Guide Of Automatic Grease Lubrication Systems

What Are the Benefits of Automatic Lubrication Systems?

Automatic lubrication provides several potential maintenance benefits when correctly designed and maintained.

Consistent Lubrication

The system can deliver controlled quantities of lubricant at scheduled intervals. This can help reduce the risk of inconsistent manual lubrication.

Reduced Manual Maintenance

Technicians do not need to manually visit every lubrication point as frequently. This can save maintenance time, particularly on equipment with numerous lubrication points.

Better Access to Difficult Areas

Automatic lubrication can serve components located in areas that are elevated, enclosed, hot, contaminated, or difficult to reach safely.

Reduced Risk of Over-Lubrication

Applying too much lubricant can be as problematic as applying too little. Metering devices can help control lubricant quantities and intervals.

Improved Maintenance Planning

Many modern systems can be integrated with monitoring or control equipment. This can help maintenance teams identify lubrication-related issues and plan service activities.

Also Read: Common Mistakes in Automatic Lubrication Installation

How Do You Choose the Right Automatic Lubrication System?

Choosing a system requires more than simply counting lubrication points. Consider:

Number of Lubrication Points

A single-point lubricator may work for one bearing, while a large centralized system may be more appropriate for equipment with dozens or hundreds of lubrication points.

Lubricant Type

Determine whether the application requires grease, oil, or another approved lubricant.

Operating Environment

Temperature, dust, moisture, vibration, washdown conditions, and outdoor exposure can influence system selection.

This is particularly important for equipment operating in Canadian winters or demanding industrial environments across the United States, where temperature conditions can vary significantly.

Distance Between Components

Large machines may require a system capable of delivering lubricant over longer distances.

Equipment Operating Schedule

Continuously operating equipment may benefit from automatic lubrication because lubrication can occur while the machine follows its normal operating schedule, subject to proper system design and safety procedures.

Monitoring Requirements

For critical equipment, consider whether the lubrication system should provide pressure, level, cycle, or fault monitoring.

Must Read: Automatic Lubrication Systems for Heavy Machinery USA

Automatic Lubrication Systems for U.S. and Canadian Industries

Industries throughout the United States and Canada use automatic lubrication solutions to support equipment maintenance in demanding operating environments.

Applications can include mining, construction, manufacturing, agriculture, transportation, material handling, energy, and industrial processing.

In mining and heavy equipment, automatic lubrication can reduce the need for technicians to manually access multiple lubrication points. In manufacturing plants, centralized systems can help maintain consistent lubrication across production machinery.

Cold-weather operation also deserves attention in Canada and northern U.S. regions. Lubricant viscosity, pump performance, line routing, and component selection should match the expected operating temperatures.

Final Thoughts

So, how many types of automatic lubrication systems are there? The main types include single-line, dual-line, progressive, and single-point systems, while circulating oil and specialized lubrication systems serve additional industrial applications.

The right choice depends on the number of lubrication points, lubricant type, equipment design, operating environment, temperature, distance, and maintenance requirements. A properly designed system can make lubrication more consistent and reduce the amount of routine manual work required from maintenance teams.

For automatic lubrication systems, pumps, dispensing equipment, and fluid-management solutions for industrial applications in the United States and Canada, explore the available solutions from Micro-Lube and contact the company for application-specific guidance.

Frequently Asked Questions

1. What are the main types of automatic lubrication systems?

The main types include single-line, dual-line, progressive, and single-point lubrication systems. Circulating oil systems and specialized oil-air systems are also used for specific industrial applications.

2. Which automatic lubrication system is best for large equipment?

Dual-line or other centralized systems may be suitable for large equipment with many lubrication points. The appropriate choice depends on the equipment layout, lubricant, distances, operating conditions, and number of lubrication points.

3. Can automatic lubrication systems use grease and oil?

Yes. Different automatic lubrication systems are designed for grease, oil, or specific lubricant types. Always select the lubricant and equipment according to the machinery manufacturer’s requirements.

4. Are automatic lubrication systems suitable for mining equipment?

Yes. Automatic lubrication systems can be used on various mining and heavy-duty equipment where numerous lubrication points, difficult access, or demanding operating conditions make manual lubrication challenging.

5. How often should an automatic lubrication system operate?

The operating frequency depends on the equipment, lubricant, load, speed, temperature, and manufacturer’s lubrication requirements. The system should be configured to deliver the required quantity at the appropriate interval rather than using one schedule for every machine.

How to Troubleshoot an Automatic Lubrication System

Automatic lubrication systems help industrial machinery receive consistent amounts of oil or grease at predetermined intervals. They can support bearings, bushings, gears, chains, pins, and other moving components while reducing the need for frequent manual lubrication. However, like any mechanical system, an automatic lubricator can develop problems that affect lubricant delivery and equipment performance. Automatic lubrication system troubleshooting starts with identifying the symptoms, checking the lubricant supply, inspecting the pump and distribution lines, and verifying that the system’s controls and metering components operate correctly. A structured approach can help maintenance teams identify problems before they lead to unnecessary equipment downtime.

For industrial facilities across the USA and Canada, troubleshooting becomes especially important when machinery operates continuously, under heavy loads, in dusty environments, or through significant seasonal temperature changes.

How Does an Automatic Lubrication System Work?

Before troubleshooting a problem, it helps to understand the basic operating process.

A typical automatic lubrication system includes a lubricant reservoir, pump, controller or timer, distribution lines, metering devices, and lubrication points. Depending on the system design, the pump moves oil or grease from the reservoir through the distribution network. Metering components then control how much lubricant reaches individual points.

Micro-Lube’s automatic lubrication information describes systems that use components such as pumps, distribution lines, metering devices, and control systems to deliver lubricant to targeted machine components.

When one part of this chain does not work correctly, the entire lubrication process can become inconsistent.

Common Automatic Lubrication System Problems

1. The Pump Is Not Operating

If the pump does not activate, the first step is to determine whether the problem is electrical, mechanical, or related to the control system.

Check:

  • Power supply
  • Electrical connections
  • Fuses or circuit protection
  • Controller settings
  • Pump motor operation
  • Reservoir level
  • Visible damage or unusual noise

For electrically powered systems, verify that the system receives the correct voltage according to the manufacturer’s specifications. Do not bypass electrical safety devices simply to make the pump operate.

If the controller is functioning but the pump does not respond, the pump or its electrical circuit may require further inspection.

2. Lubricant Is Not Reaching the Lubrication Points

A functioning pump does not necessarily mean that lubricant is reaching the bearings or other components.

Possible causes include:

  • Blocked distribution lines
  • Damaged hoses
  • Loose fittings
  • Air trapped in the lines
  • Incorrect metering components
  • Excessively thick lubricant
  • Frozen or hardened lubricant
  • Restricted lubrication fittings

Start by checking the system from the reservoir toward the lubrication points. Look for visible leaks, damaged tubing, disconnected lines, or lubricant buildup around fittings.

If only one lubrication point is receiving little or no lubricant while others operate normally, the problem may be isolated to that branch, fitting, or metering device.

3. The Lubrication Lines Are Blocked

Blocked lines are a common cause of inconsistent lubricant delivery. Grease can harden or become difficult to move under certain operating and storage conditions. Contamination can also restrict small passages.

Inspect lines for:

  • Kinks
  • Crushing
  • Cracks
  • Hardened lubricant
  • Contamination
  • Loose connections
  • Physical damage

Do not assume that increasing pump pressure is the correct solution. Excessive pressure can damage components or create unsafe operating conditions. Follow the equipment manufacturer’s pressure limits and troubleshooting procedures.

4. The System Is Delivering Too Much Lubricant

Over-lubrication can be just as problematic as insufficient lubrication. Excess grease around a bearing can increase friction and heat, while excessive lubricant consumption may indicate incorrect settings or a metering problem.

Possible causes include:

  • Incorrect timer settings
  • Incorrect metering device
  • Excessive pump cycles
  • Incorrect lubricant volume
  • Incorrect application settings
  • A damaged metering component

Review the recommended lubricant quantity and frequency for the specific equipment. Do not simply reduce lubrication because grease appears around a component; some applications naturally purge a small amount of lubricant.

5. The System Is Delivering Too Little Lubricant

Insufficient lubrication can increase friction, wear, heat, and the risk of premature component failure.

Possible causes include a low reservoir level, blocked lines, incorrect metering, insufficient pump operation, leaks, or lubricant that does not suit the application.

Look for warning signs such as:

  • Increased bearing temperature
  • Unusual noise
  • Higher vibration
  • Visible wear
  • Dry or poorly lubricated components
  • Reduced equipment performance

Micro-Lube also identifies inadequate lubrication, blocked lines, incorrect lubricant selection, and pump or electrical problems among potential causes of lubrication-system problems.

6. Air Is Entering the Lubrication System

Air can interfere with consistent lubricant delivery, particularly in systems that require reliable flow through relatively long distribution lines.

If the system produces intermittent delivery, inspect connections and fittings for potential air-entry points. Check the reservoir and pump connection, and follow the manufacturer’s recommended priming procedure.

Avoid introducing additional air during lubricant filling. Clean filling equipment and proper lubricant-handling practices can help maintain consistent system operation.

7. The Lubricant Is Not Suitable

Lubricant selection plays an important role in automatic lubrication performance.

A lubricant that is too thick for the system may create excessive resistance and restrict delivery. A lubricant that does not meet the equipment requirements may also provide inadequate protection.

Before changing lubricant, verify:

  • Required viscosity or grease consistency
  • Operating temperature range
  • Equipment manufacturer’s recommendations
  • Compatibility with seals and system components
  • Pump and metering-system requirements

Do not mix different greases or oils unless compatibility has been confirmed.

8. Cold Weather Is Affecting Lubricant Flow

Temperature can have a major effect on lubricant behavior. This is particularly relevant for equipment operating through cold winters in regions of Canada and thautomatic lubricatione northern United States.

Grease and oil can become more viscous as temperatures fall. As a result, pumps may require more effort to move the lubricant, while distribution lines may experience increased resistance.

For cold-weather applications, review the lubricant’s operating-temperature range and ensure that the automatic lubrication system is suitable for the expected conditions.

9. The Controller or Timer Is Incorrectly Configured

An automatic lubrication system depends on correct timing or control settings. If the controller is incorrectly programmed, the equipment may receive lubricant too frequently or not frequently enough.

Check:

  • Lubrication interval
  • Pump cycle duration
  • Alarm settings
  • Operating mode
  • Sensor inputs
  • System clock or timing configuration

When troubleshooting, record the original settings before making changes. This creates a useful reference if the system needs to be returned to its previous configuration.

A Practical Automatic Lubrication System Troubleshooting Checklist

When a system is not operating correctly, maintenance personnel can follow a logical sequence:

Step 1: Check the lubricant reservoir. Confirm that sufficient oil or grease remains and inspect the lubricant for contamination or abnormal condition.

Step 2: Check the power and controller. Verify that the system receives power and that the controller or timer operates normally.

Step 3: Inspect the pump. Check whether the pump activates during a normal lubrication cycle.

Step 4: Inspect distribution lines. Look for leaks, kinks, disconnected fittings, blockages, and physical damage.

Step 5: Check metering components. Confirm that metering devices are appropriate for the application and functioning correctly.

Step 6: Verify lubricant delivery. Determine whether lubricant reaches the intended lubrication points.

Step 7: Inspect the machine. Check bearings, bushings, gears, pins, and other components for signs of inadequate or excessive lubrication.

Step 8: Review system settings. Compare timing and delivery settings with the equipment manufacturer’s recommendations.

How Preventive Maintenance Reduces Lubrication Problems

Troubleshooting should not replace routine maintenance. Regular inspection can identify small problems before they become equipment failures.

Useful practices include:

  • Inspecting lubricant lines regularly
  • Checking reservoir levels
  • Keeping filling equipment clean
  • Monitoring lubricant consumption
  • Inspecting fittings and connections
  • Checking system alarms
  • Reviewing pump operation
  • Monitoring bearing temperature and vibration
  • Replacing damaged components promptly
  • Maintaining accurate service records

Micro-Lube also recommends regular system inspections during equipment downtime and periodically running systems when appropriate to help prevent lubricant hardening and line blockage.

Automatic Lubrication in USA and Canada Industrial Applications

Automatic lubrication systems are used across manufacturing, construction, mining, agriculture, transportation, and other industrial applications. These environments can place different demands on lubrication equipment, from continuous production schedules to heavy loads, dust, vibration, and extreme temperatures.

In Western Canada, for example, industrial and mining equipment may operate in demanding outdoor conditions where temperature changes can influence lubricant flow. In the USA, manufacturing plants, construction fleets, agricultural equipment, and material-handling operations may require reliable lubrication over long operating cycles.

The right troubleshooting procedure therefore depends on the specific equipment, lubrication system design, lubricant, operating environment, and manufacturer’s requirements.

When Should You Contact a Lubrication Specialist?

If basic inspections do not identify the problem, continued operation may create additional equipment damage. Professional assistance may be appropriate when:

  • The pump repeatedly fails
  • System pressure behaves unexpectedly
  • Lubricant cannot reach multiple lubrication points
  • Electrical faults continue
  • Components repeatedly clog
  • Bearings show signs of severe lubrication failure
  • The system requires major component replacement
  • The correct lubricant or settings are uncertain

A specialist can evaluate the complete lubrication circuit rather than focusing on only one component.

Frequently Asked Questions

What is the most common automatic lubrication system problem?

Common issues include low lubricant levels, blocked or damaged lines, pump problems, incorrect settings, lubricant incompatibility, and metering-component problems. The actual cause depends on the system and application.

Why is my automatic lubrication system not pumping grease?

Check the reservoir level, power supply, pump operation, lubricant condition, and distribution lines. A blockage or unsuitable lubricant can also prevent proper delivery.

How do I know if my automatic lubrication system is working?

Check whether the pump cycles correctly, lubricant moves through the distribution system, and the intended lubrication points receive the appropriate amount. Equipment temperature, noise, vibration, and lubricant consumption can also provide useful clues.

Can cold temperatures affect automatic lubrication?

Yes. Low temperatures can increase lubricant viscosity and make pumping and distribution more difficult. Cold-weather applications should use a lubricant and system configuration appropriate for the expected temperature range.

How can I prevent automatic lubrication system failures?

Regularly inspect the pump, reservoir, lines, fittings, metering components, and controller. Use the correct lubricant, maintain clean filling practices, monitor system performance, and follow the equipment manufacturer’s maintenance recommendations.

Conclusion

Effective automatic lubrication system troubleshooting starts with understanding how lubricant moves from the reservoir to each lubrication point. Problems with the pump, power supply, controller, lubricant, metering devices, fittings, or distribution lines can all affect delivery.

For industrial operations throughout the USA and Canada, regular inspections and preventive maintenance can help identify lubrication problems before they contribute to costly equipment damage or unplanned downtime. A properly selected and maintained automatic lubrication system can provide consistent lubricant delivery while supporting reliable machinery operation.

Micro-Lube provides lubrication, filtration, and fluid-management solutions for industrial applications. If you are experiencing recurring lubrication problems, evaluating a new system, or looking for support with your existing equipment, contact Micro-Lube to discuss your application and lubrication requirements.

Automatic Fuel Nozzles vs Manual Nozzles: Key Differences

Fuel dispensing equipment plays an important role in fleet operations, construction sites, agricultural facilities, mining operations, workshops, and industrial facilities. The fuel nozzle is one of the most frequently used components in a fuel transfer system because it controls the flow of fuel from the pump or dispensing system into the vehicle or equipment tank. When choosing a fuel nozzle, two common options are automatic fuel nozzles vs manual fuel nozzles. Although both perform the same basic function—dispensing fuel safely and efficiently—they differ in operation, convenience, control, and application.

Understanding the difference between automatic and manual nozzles can help businesses select the right equipment for their fuel dispensing requirements.

What Is a Fuel Nozzle?

A fuel nozzle is a dispensing device connected to a fuel transfer pump or dispensing system. It allows an operator to control the flow of fuel while filling a tank.

  fuel nozzle

The nozzle provides the final point of control between the fuel transfer system and the equipment being refueled. Choosing a suitable nozzle can improve handling, reduce spills, and make routine fueling easier.

What Is an Automatic Fuel Nozzle?

An automatic fuel nozzle is designed to help control fuel flow during dispensing. Many automatic nozzles include an automatic shut-off mechanism that stops fuel flow when the receiving tank reaches its fill level.

This feature reduces the need for the operator to continuously monitor the fuel level during dispensing. Depending on the nozzle design and application, automatic nozzles may also provide multiple flow positions, allowing operators to select a suitable dispensing rate.

Automatic nozzles are commonly used with fuel transfer systems for:

  • Fleet vehicles
  • Construction equipment
  • Agricultural machinery
  • Industrial equipment
  • Mining equipment
  • Service stations
  • Bulk fuel dispensing systems

Their combination of flow control and automatic shut-off makes them useful for operations where operators refuel equipment frequently.

What Is a Manual Fuel Nozzle?

A manual fuel nozzle requires the operator to control the fuel flow directly throughout the dispensing process. The operator typically squeezes or releases the nozzle handle to start, adjust, or stop fuel flow.

Manual nozzles provide straightforward operation and can work well in applications where the operator needs direct control over the dispensing process.

They are often used for:

  • Workshops
  • Small fleets
  • Agricultural facilities
  • Machinery maintenance areas
  • Equipment service locations
  • General-purpose fuel transfer

Because manual nozzles rely more heavily on operator control, the user needs to monitor the tank during refueling and stop the flow when the required amount has been delivered.

Automatic vs Manual Fuel Nozzles: Key Differences

The biggest difference between these two nozzle types is how they control fuel flow.

Feature Automatic Fuel Nozzle Manual Fuel Nozzle
Flow control Operator-controlled with automatic shut-off Directly controlled by operator
Automatic shut-off Typically available Generally not included
Operator monitoring Reduced during normal filling Requires continuous attention
Ease of use Convenient for frequent fueling Simple and straightforward
Spill-control support Automatic shut-off can help reduce overfilling Depends more on operator control
Best suited for High-frequency and commercial fueling Controlled, general-purpose applications
Operation More automated More manual

The exact features vary by manufacturer and nozzle model, so users should always check the specifications before selecting equipment.

Benefits of Automatic Fuel Nozzles

1. Automatic Shut-Off

One of the main advantages of an automatic nozzle is its shut-off mechanism. When the nozzle senses that the tank is reaching its fill point, it can stop the fuel flow.

This can help reduce overfilling and unnecessary fuel spills when the nozzle is correctly positioned and operated.

2. Convenient Fuel Dispensing

Automatic nozzles can make repetitive fueling tasks more convenient. Fleet operators, maintenance teams, and equipment operators may refuel several machines during a workday. A nozzle with automatic shut-off can reduce the amount of continuous monitoring required during each filling cycle.

3. Better Operator Efficiency

When a business handles frequent fueling, small improvements in each fueling task can make a difference to daily workflow. Automatic nozzles can simplify routine dispensing and allow operators to focus on other parts of the fueling process.

4. Useful for High-Volume Applications

Operations that regularly refuel trucks, construction equipment, agricultural machinery, or industrial equipment may benefit from automatic nozzles because they support consistent and convenient fuel dispensing.

Benefits of Manual Fuel Nozzles

1. Simple Operation

Manual nozzles have a straightforward design. The operator controls the flow using the nozzle handle, making the equipment easy to understand and operate.

2. Direct Control

Some applications require the operator to control fuel flow carefully. A manual nozzle provides direct control over when dispensing starts and stops.

3. Suitable for Smaller Operations

If a facility only refuels equipment occasionally, a manual nozzle may provide the functionality needed without additional automatic features.

4. Flexible Fueling

Manual operation can be useful when the operator needs to adjust the flow according to the equipment, tank size, or fueling conditions.

Which Fuel Nozzle Should You Choose?

The right nozzle depends on your fuel type, pump capacity, operating environment, equipment requirements, and fueling frequency.

An automatic fuel nozzle may be appropriate when:

  • Equipment requires frequent refueling.
  • Operators want automatic shut-off functionality.
  • The facility handles multiple vehicles or machines.
  • Reducing overfilling is an important consideration.
  • The business operates a high-use fuel dispensing system.

A manual nozzle may be suitable when:

  • Fueling occurs less frequently.
  • The operator needs direct control of fuel flow.
  • The application is relatively simple.
  • The facility uses a basic fuel transfer system.
  • Operators can continuously monitor the filling process.

It is also important to match the nozzle with the fuel transfer pump, hose, fittings, flow requirements, and fuel compatibility.

What Should You Check Before Buying a Fuel Nozzle?

Before purchasing a nozzle, consider more than just whether it is automatic or manual.

Fuel Compatibility

Confirm that the nozzle materials and seals are compatible with the fuel being dispensed. Compatibility can affect service life and safe operation.

Flow Rate

Check the required fuel flow rate. A nozzle should work effectively with the capacity of the connected fuel transfer pump and hose.

Connection Size

Make sure the nozzle connection matches the hose and other components in the dispensing system. An incorrect connection can create installation and performance problems.

Operating Environment

Consider where the nozzle will be used. Mining, construction, agricultural, fleet, and industrial environments may expose equipment to dust, moisture, vibration, or frequent handling.

Ergonomics

Operators may use a fuel nozzle many times each day. A comfortable handle, suitable weight, and easy-to-operate trigger can make routine fueling more convenient.

Shut-Off Design

If you select an automatic nozzle, understand how its automatic shut-off system operates and follow the manufacturer’s installation and operating instructions.

Safety Tips for Using Fuel Nozzles

Regardless of whether you use an automatic or manual nozzle, proper operating practices remain essential.

Always:

  • Inspect the nozzle, hose, and connections before use.
  • Check for leaks or visible damage.
  • Use equipment compatible with the fuel being dispensed.
  • Keep ignition sources away from fueling areas.
  • Avoid overfilling tanks.
  • Maintain good ventilation where required.
  • Follow the manufacturer’s operating instructions.
  • Secure hoses and dispensing equipment when not in use.
  • Replace damaged components promptly.
  • Train operators on proper fuel dispensing procedures.

An automatic shut-off feature provides an additional control mechanism, but it does not eliminate the need for operator attention and safe fueling practices.

Automatic Fuel Nozzles for Industrial and Heavy-Duty Applications

Industrial facilities, fleet operators, mining companies, construction businesses, and agricultural operations often need dependable equipment for transferring and dispensing fuel. In these environments, the nozzle needs to work as part of a complete fuel transfer system rather than as an isolated component.

The pump, hose, nozzle, meter, fittings, filters, and storage equipment should work together according to the requirements of the application.

For frequent fueling operations, an automatic fuel nozzle can provide convenient flow control and automatic shut-off functionality. For applications where direct operator control is the priority, a manual nozzle can offer a simple and practical solution.

Frequently Asked Questions

Are automatic fuel nozzles better than manual nozzles?

They serve different applications. Automatic nozzles offer features such as automatic shut-off, while manual nozzles provide direct operator control. The appropriate choice depends on the fueling system and operating requirements.

Do automatic fuel nozzles stop fuel automatically?

Many automatic fuel nozzles include an automatic shut-off mechanism that stops dispensing when the nozzle detects the tank has reached its fill level. Correct nozzle positioning and proper operation remain important.

Can automatic nozzles be used for diesel fuel?

Many automatic nozzles are designed for diesel and other compatible fuels, but compatibility varies by model. Always verify the manufacturer’s specifications before use.

What is the main advantage of a manual fuel nozzle?

The main advantage is direct control. The operator can start, adjust, and stop fuel flow manually according to the fueling requirements.

What should I consider when buying a fuel nozzle?

Consider fuel compatibility, flow rate, connection size, pump capacity, operating environment, construction quality, nozzle design, and whether automatic shut-off functionality is required.

Are automatic nozzles suitable for fleet fueling?

They can be suitable for fleet fueling because automatic shut-off and convenient flow control can simplify frequent refueling. The nozzle should still match the fuel, pump, hose, and operating conditions.

Final Thoughts

Automatic and manual fuel nozzles both have an important role in fuel dispensing systems. Automatic fuel nozzles can provide added convenience and automatic shut-off functionality, making them useful for frequent and high-volume fueling applications. Manual fuel nozzles provide straightforward operation and direct control, which can work well for simpler fueling requirements.

The best choice depends on your fuel type, dispensing volume, pump capacity, equipment, operating environment, and safety requirements. Selecting a compatible, properly rated nozzle can help create a reliable and efficient fuel transfer setup.

For reliable fuel dispensing equipment, automatic fuel nozzles, fuel transfer pumps, hoses, and fluid handling solutions, explore the solutions available from Micro Lube. Contact the team to discuss your application and identify equipment that fits your fuel transfer requirements.

How Can Fluid Management Systems Reduce Maintenance Costs?

Industrial facilities depend on lubricants, hydraulic fluids, coolants, and other service fluids to keep machinery operating efficiently. However, managing these fluids manually can create unnecessary costs through overuse, contamination, inaccurate inventory records, spills, inefficient dispensing, and unexpected equipment downtime. A fluid management system provides a more organized approach to storing, monitoring, transferring, dispensing, and tracking industrial fluids. For businesses across the United States and Canada, these systems can help maintenance teams improve fluid control, reduce waste, protect equipment, and make maintenance operations more efficient.

From manufacturing plants and mining operations to fleet maintenance facilities, construction companies, agriculture, and heavy equipment workshops, better fluid management can contribute directly to lower operating and maintenance costs.

What Is a Fluid Management System?

A fluid management system is a combination of equipment and technology used to control how industrial fluids are stored, transferred, dispensed, monitored, and tracked.

Depending on the application, a system may include:

  • Storage tanks and containers
  • Oil and grease pumps
  • Filtration equipment
  • Hose reels
  • Flow meters
  • Dispensing equipment
  • Control valves
  • Fluid monitoring systems
  • Inventory management technology
  • Automatic alerts and reordering functions

The goal is to ensure that the right fluid reaches the right equipment in the right quantity while maintaining better control over inventory and usage.

Modern fluid management solutions can provide much more visibility than traditional drums, pails, and manual dispensing methods.

How Can Fluid Management Systems Reduce Maintenance Costs?

1. Reduce Lubricant Waste

One of the simplest ways a fluid management system can reduce costs is by controlling how much lubricant is dispensed.

Manual fluid handling can make it difficult to know exactly how much oil or other service fluid is being used. Over-dispensing can increase consumption without providing additional equipment benefits.

Controlled dispensing and metering allow maintenance teams to deliver more consistent quantities. This can reduce unnecessary lubricant usage and make consumption easier to monitor.

For large facilities where hundreds or thousands of gallons of lubricant are used annually, even small reductions in waste can have a meaningful financial impact.

2. Improve Fluid Inventory Control

Poor inventory management creates two costly problems: businesses may overstock fluids or run out of essential lubricants when they need them.

A fluid management system can provide better visibility into fluid inventory and usage. Advanced monitoring systems can track consumption and provide alerts when supplies need attention.

Micro Lube’s NEX.U. fluid monitoring solution, for example, is designed to help businesses account for lubricant usage, control inventory, and receive automatic alerts and fluid reordering information.

Better inventory visibility can help maintenance departments avoid emergency purchases, unnecessary stock, and fluid-related interruptions.

3. Minimize Fluid Contamination

Contaminated lubricant can contribute to equipment wear and premature component failure.

Dust, dirt, moisture, particles, and other contaminants can enter fluids during storage, transfer, or dispensing. Once contaminated fluid enters sensitive equipment, it can affect bearings, pumps, hydraulic components, gears, and other machinery.

A well-designed fluid management system can incorporate filtration and controlled transfer methods to help maintain fluid cleanliness.

Micro Lube also offers lubrication work-center solutions featuring dedicated pumps and filters for individual tanks, helping prevent cross-contamination between lubricants.

Reducing contamination can help protect equipment and potentially reduce maintenance expenses associated with premature component replacement.

4. Protect Expensive Industrial Equipment

Lubricants are essential for reducing friction, controlling heat, protecting components, and supporting reliable machine operation.

When the wrong lubricant is used, the fluid is contaminated, or lubrication quantities are inconsistent, equipment can experience unnecessary wear.

A fluid management system helps create a more controlled process for handling lubricants and service fluids. Better control can support equipment reliability and reduce the likelihood of fluid-related maintenance problems.

This is particularly important for high-value equipment used in:

  • Mining
  • Manufacturing
  • Construction
  • Agriculture
  • Transportation
  • Fleet maintenance
  • Power generation
  • Heavy equipment operations

5. Reduce Unplanned Downtime

Unexpected equipment downtime can cost significantly more than the price of the failed component itself. Production interruptions, emergency labor, replacement parts, and delayed operations can quickly increase the total cost of a maintenance event.

Better fluid management can support preventive maintenance by ensuring that lubricants and other service fluids are available, properly stored, clean, and dispensed consistently.

For businesses operating continuous-production facilities or large equipment fleets, preventing even a small number of fluid-related failures can provide substantial operational value.

6. Improve Maintenance Technician Productivity

Manual fluid handling often requires technicians to locate containers, transport fluids, connect equipment, measure quantities, and clean up spills.

A centralized or organized fluid management system can simplify these tasks.

For example, dedicated dispensing stations and hose reels can make fluids easier to access and transfer. Properly organized equipment can reduce unnecessary movement and help technicians spend more time on maintenance activities that directly support equipment reliability.

Micro Lube’s product range includes pumps, hose reels, filtration systems, storage and dispensing equipment, meters, control valves, and other fluid-management products designed for industrial applications.

7. Improve Lubricant Accountability

Do you know how much oil your facility uses every month? Do you know which machine received it and when?

Without accurate tracking, lubricant losses can be difficult to identify.

Fluid monitoring technology can provide greater visibility into fluid consumption. This information can help maintenance managers identify unusual usage patterns, investigate waste, and make more informed purchasing decisions.

8. Reduce Spills and Improve Workplace Organization

Manual fluid transfer can increase the possibility of spills, leaks, and poorly stored containers.

Spills create cleanup requirements and can create additional workplace and environmental-management concerns.

Proper storage and dispensing equipment can help organize fluid handling and reduce unnecessary exposure during transfer.

For example, purpose-designed lubrication work centers can incorporate storage, dispensing areas, filtration, spill containment, and organized equipment in a single solution.

A cleaner and more organized maintenance area can also make routine service work easier and more efficient.

Fluid Management for USA and Canada Industries

The benefits of fluid management apply across many industries throughout North America.

Manufacturing

Manufacturing facilities often operate multiple machines that require different lubricants. Controlled storage and dispensing can help reduce cross-contamination and improve lubricant availability.

Mining

Mining equipment operates under heavy loads and demanding environmental conditions. Reliable fluid transfer and lubrication practices can help maintenance teams protect expensive machinery.

Construction

Construction equipment frequently works in dusty environments and requires regular servicing. Efficient fluid handling can make routine maintenance faster and more organized.

Agriculture

Tractors, harvesters, loaders, and other agricultural equipment depend on reliable lubrication and fluid maintenance. Better inventory and dispensing control can help reduce waste during busy operating seasons.

Fleet and Transportation

Fleet maintenance facilities may manage engine oils, hydraulic fluids, transmission fluids, greases, and other service products. Accurate dispensing and inventory tracking can simplify maintenance operations across multiple vehicles.

How to Choose a Fluid Management System

The right solution depends on your operation’s size, the fluids you handle, your equipment requirements, and your maintenance goals.

Before selecting a system, consider:

  1. Types of fluids: Identify the oils, greases, hydraulic fluids, coolants, or other fluids being managed.
  2. Required storage capacity: Determine how much fluid your operation normally consumes.
  3. Filtration requirements: Consider whether the fluid needs to be filtered before dispensing.
  4. Dispensing accuracy: Determine whether flow meters or controlled dispensing are required.
  5. Inventory monitoring: Consider whether automated tracking and alerts would improve inventory control.
  6. Contamination prevention: Evaluate how fluids are currently stored and transferred.
  7. Future requirements: Select equipment that can support changing maintenance and operational needs.

Final Thoughts

A fluid management system can help reduce maintenance costs by improving lubricant control, reducing waste, minimizing contamination, improving inventory visibility, and supporting more efficient maintenance operations.

For industrial businesses across the USA and Canada, the financial benefits can extend beyond the cost of the lubricant itself. Better fluid management can help protect valuable equipment, reduce avoidable downtime, improve technician productivity, and provide maintenance teams with better information for planning and decision-making.

Micro Lube provides industrial fluid management, lubrication, filtration, storage, dispensing, pumps, meters, and fluid-transfer solutions for demanding applications. If your business is looking to improve lubricant control and reduce maintenance-related costs, contact Micro Lube to discuss a fluid management solution suited to your equipment and operation.

5 Critical Lubrication Mistakes That Are Damaging Your Machinery

Industrial machinery is built to operate reliably under demanding conditions, but even high-quality equipment can suffer premature wear when lubrication mistakes are made or lubrication is not managed correctly. Bearings, gears, chains, compressors, pumps, motors, hydraulic equipment, and other moving components depend on the right lubricant, applied in the right quantity and at the right time.

Lubrication is more than simply adding oil or grease to a machine. A lubricant helps reduce friction and wear, manage heat, protect surfaces from corrosion, and support smooth equipment operation. When lubrication practices are incorrect, the result can be overheating, component damage, unplanned downtime, higher maintenance costs, and shortened equipment life.

For industrial facilities across the United States and Canada, developing a disciplined lubrication program is an important part of preventive and predictive maintenance. Here are five common lubrication mistakes that can quietly damage machinery and reduce operational reliability.

1. Using the Wrong Lubricant

One of the most serious lubrication mistakes is selecting a lubricant simply because it is available or because it worked on another machine.

Different components have different lubrication requirements. Bearings, gears, chains, compressors, hydraulic systems, and electric motors may require different lubricant formulations, viscosities, additive packages, or grease characteristics.

Using the wrong product can result in inadequate film strength, excessive friction, overheating, poor protection, or incompatibility with seals and other materials.

How to avoid it

Always consult the equipment manufacturer’s lubrication specifications before selecting a product. Consider:

  • Required viscosity
  • Operating temperature
  • Load and speed
  • Application method
  • Lubricant type
  • Additive requirements
  • Environmental conditions
  • Compatibility with existing lubricant

A lubricant should be selected according to the application rather than based only on brand, price, or appearance.

2. Over-Lubricating Machinery

More lubricant does not necessarily mean better protection.

Over-lubrication is particularly common with bearings and grease-lubricated components. Excess grease can increase resistance inside a bearing, generate additional heat, cause seal problems, and potentially lead to premature component failure. It can also increase lubricant consumption and maintenance costs.

Industry guidance emphasizes that both under-lubrication and over-lubrication can create problems. The objective is to deliver the correct amount at the appropriate interval.

How to avoid it

Establish a defined lubrication quantity for each lubrication point. Do not rely solely on habit or visual inspection.

For critical machinery, maintenance teams can use calculated relubrication quantities, manufacturer recommendations, condition monitoring, temperature checks, and appropriate lubrication equipment to improve consistency.

The goal should always be the right lubricant, in the right amount, at the right time.

3. Under-Lubricating or Skipping Lubrication Intervals

At the opposite end of the problem is insufficient lubrication.

When a component does not receive enough lubricant, the protective film between moving surfaces may become inadequate. This can increase friction and wear and generate excessive heat.

Under-lubrication can be especially damaging in bearings, gears, chains, and other continuously moving components. In severe cases, insufficient lubrication can contribute to component seizure and unexpected equipment failure.

How to avoid it

Create a documented lubrication schedule based on equipment requirements and operating conditions.

A good lubrication program should identify:

  • Equipment and asset number
  • Lubrication points
  • Lubricant specification
  • Required quantity
  • Application method
  • Lubrication frequency
  • Maintenance responsibility
  • Inspection requirements

Modern facilities can also use condition monitoring and automated lubrication systems where appropriate to improve consistency and reduce missed lubrication points.

4. Mixing Incompatible Lubricants

Another potentially costly mistake is mixing different oils or greases without confirming compatibility.

Two lubricants may appear similar but contain different base oils, thickeners, additives, or performance characteristics. Mixing incompatible greases can alter consistency and reduce the lubricant’s ability to protect the component.

Similarly, changing from one industrial oil to another without an appropriate transition procedure may create compatibility or performance concerns.

How to avoid it

Before changing lubricants:

  1. Identify the lubricant currently in use.
  2. Review the manufacturer’s specifications.
  3. Confirm compatibility with the replacement product.
  4. Clean or flush the system when required.
  5. Label lubricant containers clearly.
  6. Store different products separately.
  7. Train maintenance personnel on lubricant identification.

A centralized lubricant management program can help prevent accidental cross-contamination and product mix-ups.

5. Allowing Contamination to Enter the Lubricant

Clean lubricant can become contaminated during storage, transportation, transfer, or application.

Common contaminants include dirt, dust, water, metal particles, and other foreign materials. Once contaminants enter a lubricant, they can circulate through machinery and contribute to abrasive wear, corrosion, and lubricant degradation.

This is particularly important in industrial environments where equipment may operate outdoors, around dust, moisture, chemicals, or heavy production activity.

How to avoid it

Good lubricant storage and handling practices are essential.

Keep containers sealed when not in use and store them in a clean, dry environment. Use dedicated and clean dispensing equipment. Avoid leaving open containers exposed to dust or moisture.

For circulating oil systems, filtration and oil conditioning can help control particulate contamination and maintain the required cleanliness level.

Oil analysis can also provide valuable information about lubricant condition and contamination. Changes in viscosity, particle levels, water content, or wear metals can indicate developing problems before a major failure occurs.

Why Proper Lubrication Matters for Machinery Reliability

Lubrication is a fundamental part of equipment reliability because it directly influences friction, wear, temperature, corrosion protection, and component performance.

A properly managed lubricant forms a protective layer between contacting surfaces, helping reduce direct surface interaction. Lubricants can also assist with heat transfer in circulating oil applications and may help carry contaminants toward filtration systems.

For businesses in the United States and Canada, this matters across many sectors, including:

  • Manufacturing
  • Automotive production
  • Construction
  • Agriculture
  • Mining
  • Forestry
  • Food processing
  • Material handling
  • Energy
  • Transportation
  • Metalworking

Equipment failures in these industries can affect production schedules, employee productivity, maintenance budgets, and customer commitments. A proactive lubrication program can help reduce avoidable problems and support more predictable maintenance.

How to Build a Better Industrial Lubrication Program

Avoiding lubrication mistakes requires more than reminding technicians to grease equipment. A reliable program should combine proper product selection, application procedures, monitoring, documentation, and employee training.

Standardize Lubricants

Where practical, standardize approved lubricants to reduce confusion and prevent accidental product mixing. However, standardization should never override the technical requirements of individual machines.

Label Lubricants Clearly

Use clear labels and dedicated storage and dispensing equipment. Color coding or identification systems can also help maintenance teams select the correct lubricant.

Follow Manufacturer Recommendations

Equipment manufacturers provide important information about lubricant type, quantity, and intervals. These recommendations should form the foundation of the lubrication plan.

Monitor Equipment Condition

Changes in operating temperature, vibration, noise, energy consumption, or lubricant condition can indicate developing lubrication problems.

For critical assets, oil analysis and other predictive maintenance technologies can provide additional information about machine and lubricant health.

Train Maintenance Personnel

Technicians should understand why lubricant selection, quantity, contamination control, storage, and application methods matter. Training helps transform lubrication from a routine task into a structured reliability activity.

Signs Your Machinery May Have a Lubrication Problem

Recognizing early warning signs can help prevent larger failures. Potential indicators include:

  • Unusual bearing or gearbox noise
  • Excessive operating temperature
  • Increased vibration
  • Oil leakage
  • Grease leakage or purging
  • Discolored or degraded lubricant
  • Unexpected lubricant consumption
  • Metal particles in oil or grease
  • Reduced machine performance
  • Repeated component failures

These signs do not automatically mean lubrication is the only cause. However, they should trigger an inspection and condition assessment.

Frequently Asked Questions

What is the biggest lubrication mistake?

There is no single mistake that affects every machine, but using the wrong lubricant, applying too much or too little, and allowing contamination are among the most common causes of lubrication-related problems.

Can over-lubrication damage bearings?

Yes. Excessive grease can increase friction and heat and may contribute to seal or bearing problems. The correct quantity and relubrication interval should be determined from equipment requirements.

How can I prevent lubricant contamination?

Store lubricants properly, keep containers closed, use clean dispensing equipment, avoid cross-contamination, and use appropriate filtration or oil-conditioning practices for circulating oil systems.

How often should industrial machinery be lubricated?

There is no universal interval. Lubrication frequency depends on the equipment, lubricant, load, speed, temperature, environment, and manufacturer’s recommendations. Condition-based maintenance can provide additional guidance for critical equipment.

Why is lubricant selection important?

Different machines operate under different loads, speeds, temperatures, and environmental conditions. The correct lubricant is formulated to provide appropriate protection under those specific operating conditions.

Conclusion

Lubrication is one of the most important elements of industrial machinery maintenance, but simple mistakes can undermine its benefits. Using the wrong lubricant, over-lubricating, under-lubricating, mixing incompatible products, and allowing contamination into lubricants can increase wear, operating temperatures, maintenance requirements, and the risk of unexpected equipment failure.

The solution is a structured lubrication program based on correct product selection, accurate application, contamination control, scheduled maintenance, condition monitoring, and technician training. By treating lubrication as a reliability strategy rather than a routine maintenance task, industrial facilities can better protect their equipment and support long-term operational performance.

For businesses looking for dependable industrial lubricants and lubrication solutions in the United States and Canada, Micro-Lube provides products and solutions designed to support machinery maintenance, lubrication performance, and equipment reliability. Choosing the right industrial lubricant and applying it correctly can help businesses protect valuable machinery and maintain dependable operations.

What Is a Desiccant Breather and Why Does Your Oil Tank Need One?

Industrial equipment depends on clean, dry lubricants to operate efficiently and reliably. Hydraulic systems, gearboxes, compressors, lubrication systems, and oil storage tanks are constantly exposed to environmental conditions that can introduce moisture and airborne contaminants. One of the simplest ways to reduce this risk is by installing a desiccant breather.

A desiccant breather is an air filtration device fitted to an oil reservoir or tank. It allows the reservoir to exchange air as fluid levels and temperatures change while helping remove moisture and airborne particles from incoming air. This makes desiccant breathers an important part of modern industrial lubrication and contamination control.

For businesses in manufacturing, mining, construction, agriculture, transportation, and other industries, protecting lubricant quality can help support equipment reliability, reduce contamination-related maintenance, and improve overall fluid management.

What Is a Desiccant Breather?

A desiccant breather is a specialized breather designed to control the quality of air entering an oil reservoir.

Oil tanks cannot remain completely sealed because pressure changes occur during normal operation. When oil is removed, the reservoir needs to draw in air. When oil is added, the temperature rises, or the fluid expands, air may move out of the reservoir.

With a conventional vent, outside air can bring dust, dirt, humidity, and water vapor into the tank.

A desiccant breather creates a protective barrier between the reservoir and the surrounding environment. Incoming air passes through filtration media, while moisture is absorbed by a desiccant material before the air reaches the lubricant.

In simple terms:

Outside air → particulate filtration → moisture absorption → cleaner, drier air → oil reservoir

This simple process can make a significant difference in maintaining lubricant cleanliness.

Why Does an Oil Tank Need a Desiccant Breather?

Many maintenance programs focus on removing contamination after it enters a hydraulic or lubrication system. However, preventing contamination from entering in the first place is often a better strategy.

Every breathing cycle can potentially introduce environmental contaminants.

Moisture can contribute to:

  • Corrosion
  • Rust
  • Lubricant degradation
  • Reduced lubrication performance
  • Sludge formation
  • Component wear
  • Equipment reliability issues

Airborne particles such as dust and dirt can also enter reservoirs and contribute to abrasive wear in precision components.

A desiccant breather helps reduce these risks by treating the air before it enters the reservoir.

How Does a Desiccant Breather Work?

The operation of a desiccant breather is relatively simple.

1. Pressure Changes Inside the Reservoir

As the oil level, oil temperature, and equipment operating conditions change, the pressure inside the reservoir changes.

The tank must breathe to maintain an appropriate pressure balance.

2. Air Enters the Breather

When the reservoir needs air, surrounding air enters through the breather rather than directly into the tank.

3. Airborne Particles Are Filtered

The breather contains filtration media that helps capture dust and other airborne particulate contaminants.

4. Moisture Is Absorbed

The incoming air then passes through a moisture-absorbing desiccant material. This material captures water vapor before it reaches the oil reservoir.

5. Cleaner Air Enters the Tank

The filtered and dried air enters the reservoir, helping reduce the amount of moisture and particulate contamination introduced during normal breathing cycles.

When air moves out of the reservoir, the breather also allows the pressure to equalize.

What Is Desiccant Material?

A desiccant is a material capable of absorbing moisture from the surrounding air.

One of the most commonly used materials in industrial breathers is silica gel. It attracts and holds water vapor, making it useful for protecting lubricants and equipment from atmospheric moisture.

Many industrial desiccant breathers use a visual indicator that changes color as the desiccant becomes saturated. This provides maintenance personnel with a simple way to determine when the breather may need replacement.

The exact indicator color and replacement procedure depend on the specific breather design, so operators should always follow the manufacturer’s maintenance recommendations.

What Are the Benefits of a Desiccant Breather?

1. Moisture Control

Moisture contamination can negatively affect many industrial lubricants. A desiccant breather helps limit moisture entering the reservoir through the breathing process.

2. Airborne Particle Protection

Dust and dirt can enter oil reservoirs through open or poorly protected vents. A breather with particulate filtration helps reduce this contamination pathway.

3. Improved Lubricant Protection

Cleaner, drier lubricant can provide a better operating environment for pumps, gears, bearings, valves, and other components.

4. Reduced Contamination Risk

Preventing contaminants from entering the reservoir can reduce the burden placed on downstream oil filtration systems.

5. Better Preventive Maintenance

A visible breather condition indicator can provide maintenance teams with an easy inspection point during routine equipment checks.

6. Support for Longer Equipment Life

Contamination is a major contributor to wear in many industrial systems. Effective contamination control can support more reliable operation and potentially extend component service life.

Actual results depend on the equipment, lubricant, operating conditions, contamination sources, and overall maintenance program.

Where Are Desiccant Breathers Used?

Desiccant breathers can be used in many applications where lubricants or fluids are stored in reservoirs exposed to atmospheric air.

Common applications include:

  • Hydraulic oil reservoirs
  • Industrial gearboxes
  • Lubrication systems
  • Oil storage tanks
  • Fuel storage equipment
  • Mobile hydraulic equipment
  • Mining machinery
  • Construction equipment
  • Agricultural machinery
  • Manufacturing equipment
  • Power-generation equipment
  • Industrial fluid storage containers

They are especially valuable in environments with high humidity, dust, temperature fluctuations, or heavy equipment operation.

Desiccant Breather vs. Standard Breather

A standard breather allows air to move in and out of a reservoir while providing basic protection against airborne particles.

A desiccant breather goes a step further by absorbing moisture from incoming air.

The difference can be summarized simply:

Feature Standard Breather Desiccant Breather
Allows pressure equalization Yes Yes
Filters airborne particles Depending on design Yes
Absorbs moisture No Yes
Helps control humidity Limited Yes
Suitable for contamination-sensitive systems Sometimes Often preferred

For hydraulic and lubrication systems where moisture contamination is a concern, a desiccant breather can provide an additional layer of protection.

How Do You Choose the Right Desiccant Breather?

Choosing a breather should be based on the specific equipment and operating environment.

Consider the following factors:

Reservoir Size

Larger reservoirs may experience greater air exchange and may require a breather with appropriate capacity.

Airflow

Equipment with frequent fluid movement or significant temperature changes may require higher airflow capacity.

Environmental Conditions

Consider humidity, dust, outdoor exposure, temperature changes, washdown conditions, and other environmental factors.

Connection Size

The breather must be compatible with the reservoir’s mounting connection.

Moisture Capacity

Consider how much moisture the desiccant can absorb before it becomes saturated.

Physical Space

Some installations have limited clearance. A compact breather may be more appropriate where mounting space is restricted.

Application Requirements

Hydraulic reservoirs, gearboxes, oil storage tanks, and other applications may have different breathing and contamination-control requirements.

Selecting a breather based on these factors can help ensure effective protection without unnecessarily increasing maintenance costs.

When Should You Replace a Desiccant Breather?

Desiccant breathers should be inspected regularly as part of routine maintenance.

The replacement interval depends on:

  • Humidity
  • Dust levels
  • Reservoir breathing frequency
  • Operating temperature
  • Equipment usage
  • Reservoir size
  • Breather capacity
  • Environmental exposure

Many breathers include a color-changing indicator that helps identify moisture saturation.

However, maintenance teams should not rely only on a calendar-based replacement schedule. Regular visual inspection can provide a better indication of actual breather condition.

If the desiccant is saturated, the breather becomes heavily contaminated, or airflow becomes restricted, replacement may be necessary.

Can a Desiccant Breather Remove Water Already in Oil?

No.

This is an important distinction.

A desiccant breather is primarily designed to prevent moisture from entering through the reservoir’s air exchange process. It is not a substitute for an oil purification or water-removal system.

If water is already present in hydraulic oil or industrial lubricant, the appropriate fluid-cleaning method should be selected based on the type and quantity of contamination.

Desiccant breathers and oil filtration can therefore work together:

Desiccant breather: Helps prevent moisture and airborne particles from entering.

Oil filtration: Helps remove contaminants already present in the fluid.

Oil analysis: Helps identify changes in lubricant condition.

Good storage practices: Help prevent contamination before lubricant enters equipment.

Together, these practices create a stronger contamination-control strategy.

Why Are Desiccant Breathers Important for Heavy Equipment?

Heavy equipment often operates in challenging environments. Construction sites, mines, agricultural fields, manufacturing facilities, and outdoor industrial operations can expose machinery to dust, humidity, rain, and temperature fluctuations.

Hydraulic reservoirs and gearboxes can breathe continuously during equipment operation.

Without adequate protection, every breathing cycle can provide another opportunity for environmental contamination to enter the system.

Installing an appropriate desiccant breather can help reduce this contamination pathway and support cleaner lubricant management.

For equipment owners, this can be particularly valuable when hydraulic components, gearboxes, or lubrication systems are expensive to repair or difficult to access.

Desiccant Breathers and Oil Filtration Work Together

A common mistake is treating contamination control as a single filtration activity.

In reality, an effective lubrication program should address contamination from multiple directions.

For example, a facility may use:

  1. Desiccant breathers to protect reservoirs from atmospheric moisture and particles.
  2. Oil filtration systems to clean contaminated lubricant.
  3. Oil analysis to monitor fluid condition.
  4. Clean lubricant storage practices to prevent contamination before filling.
  5. Regular inspections to identify leaks, damaged breathers, and other problems.
  6. Scheduled maintenance based on actual operating conditions.

This approach can help reduce contamination at both the entry point and within the fluid system.

Frequently Asked Questions

What is the main purpose of a desiccant breather?

A desiccant breather allows an oil reservoir to breathe while helping filter airborne particles and absorb moisture from incoming air.

Is a desiccant breather necessary for every oil tank?

Not necessarily. The need depends on the application, reservoir design, environmental conditions, lubricant sensitivity, and contamination risks. It can be particularly useful for contamination-sensitive industrial equipment.

Does a desiccant breather remove moisture from hydraulic oil?

No. It primarily prevents moisture from entering through incoming air. Existing water contamination requires an appropriate fluid-treatment solution.

How often should a desiccant breather be changed?

There is no universal replacement interval. Breather life depends on environmental humidity, dust, airflow, reservoir size, and equipment operation. Inspection indicators and manufacturer recommendations should guide replacement.

Can desiccant breathers be used on gearboxes?

Yes. Desiccant breathers are commonly used on industrial gearboxes to help reduce moisture and particulate contamination entering through the gearbox breathing process.

Can a desiccant breather replace an oil filter?

No. These products perform different functions. A desiccant breather protects the reservoir from incoming airborne contamination, while an oil filter removes contaminants from the lubricant.

Are desiccant breathers useful for hydraulic systems?

Yes. Hydraulic systems can be sensitive to particulate and moisture contamination, making contamination prevention an important part of hydraulic maintenance.

Conclusion

A desiccant breather is a small component that can play a major role in industrial contamination control. By filtering incoming air and absorbing moisture before it reaches an oil reservoir, it helps protect lubricants from environmental contamination.

For manufacturers, mining companies, construction businesses, agricultural operations, and other industries, combining desiccant breathers with effective oil filtration, lubricant analysis, clean storage, and preventive maintenance can create a more comprehensive fluid-management strategy.

Micro-Lube provides industrial lubrication and fluid-management solutions designed to help businesses protect their equipment, manage lubricants, and improve maintenance practices. Choosing the right desiccant breather for your reservoir and operating environment can be an important step toward cleaner lubricants, better contamination control, and more reliable industrial equipment.
1-888-293-1763
sales@micro-lube.com
Contact us